Mary doesn’t like wearing the wrap-around-her-head earpieces found on sunglasses these days under her bicycle helmet, so I must trim them to fit:

Perhaps I won’t need an old pair to prepare the next set: a scant four inches from the hinge.
The Smell of Molten Projects in the Morning
Ed Nisley's Blog: Shop notes, electronics, firmware, machinery, 3D printing, laser cuttery, and curiosities. Contents: 100% human thinking, 0% AI slop.
Making the world a better place, one piece at a time
Mary doesn’t like wearing the wrap-around-her-head earpieces found on sunglasses these days under her bicycle helmet, so I must trim them to fit:
Perhaps I won’t need an old pair to prepare the next set: a scant four inches from the hinge.
We have, as you might expect, a Favorite Cheese Slicer of no particular provenance. Being made of cheap pot metal, it left black smudges wherever it went and, decades ago, I coated it with bright red rubbery grip material. Recently, the coating became lumpy and peeling off the loose sections revealed a definite problem:
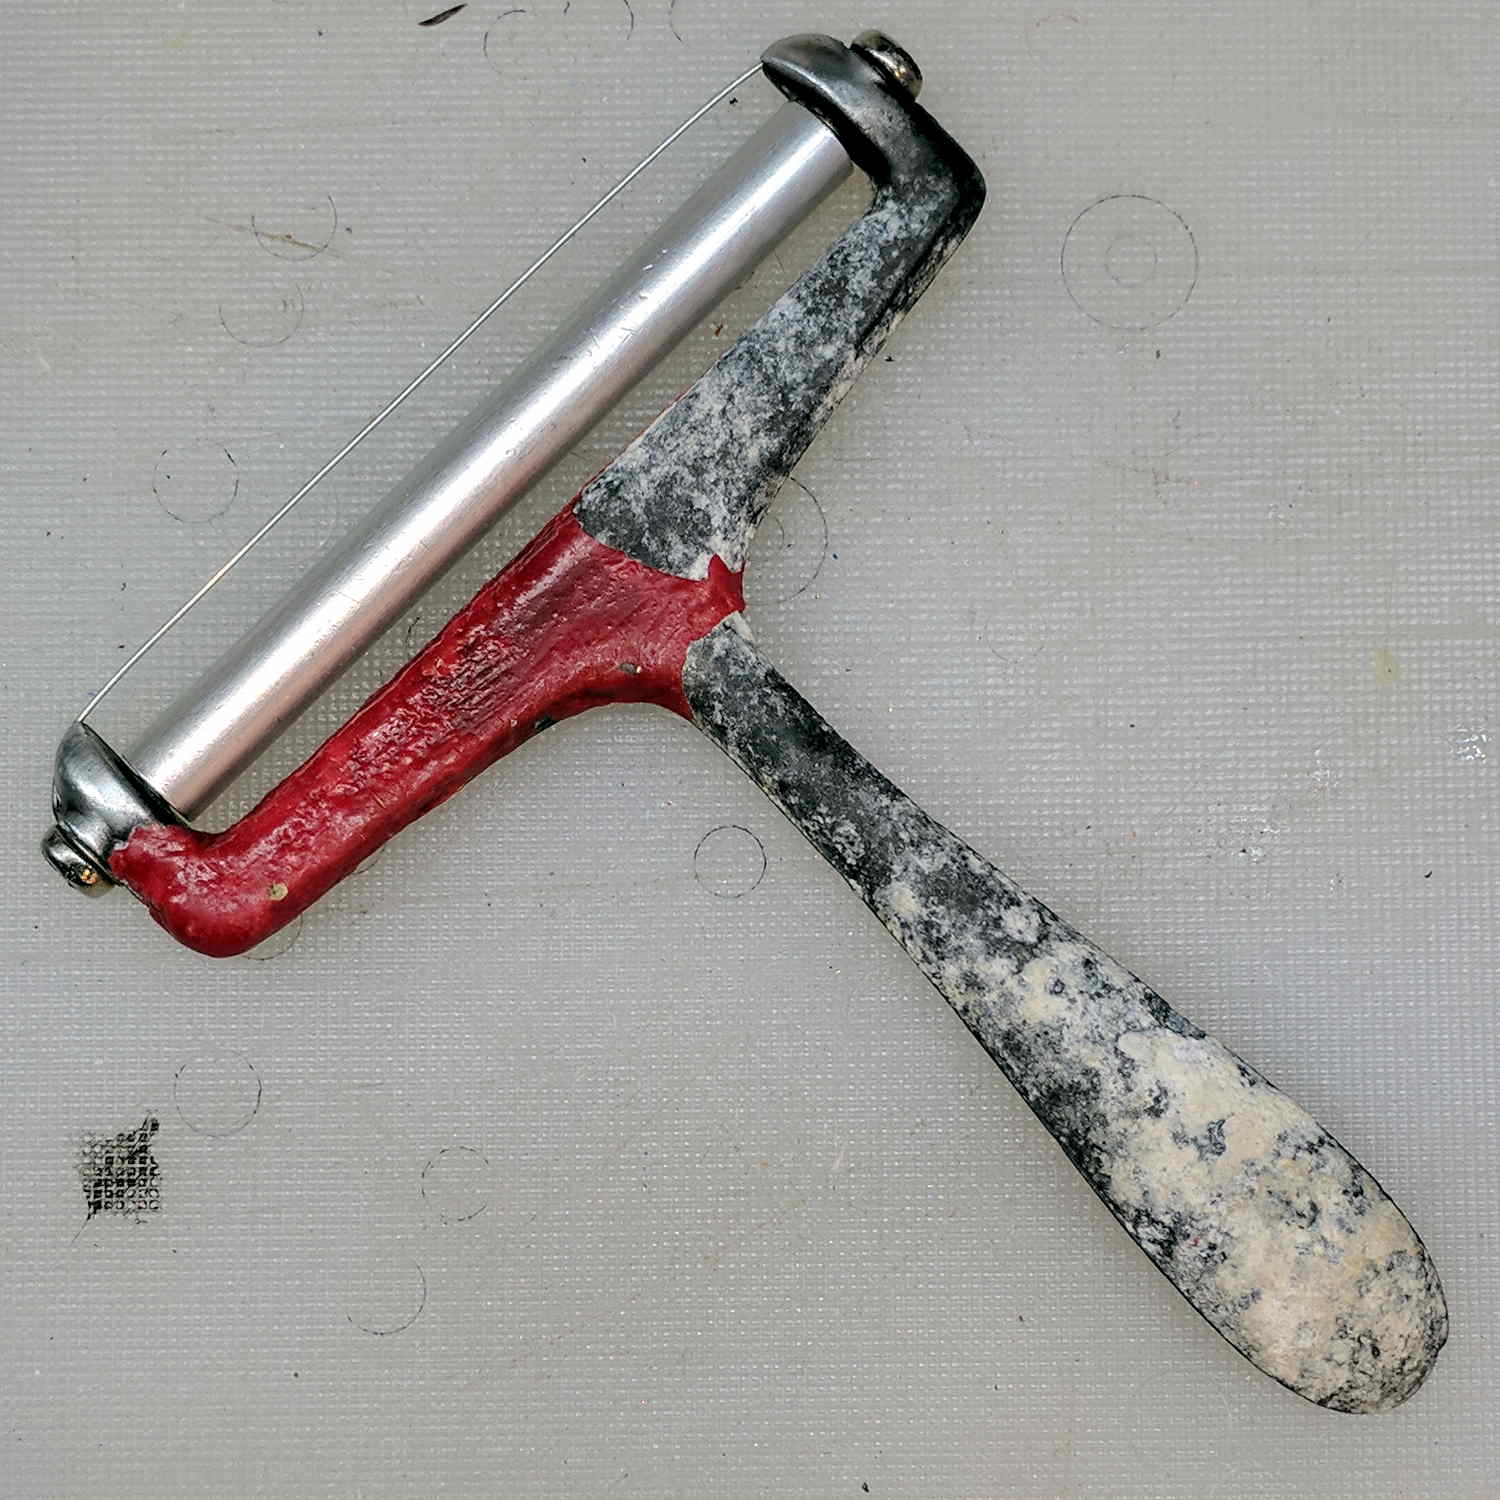
Vigorous scrubbing with a foam sanding block and a Scotchbrite pad, interspersed with rotary wire brushing, removed the corrosion and left a slightly pitted metal frame. Protip: scrub under water and wire-brush with a vacuum hose to keep the dust under control.
A pair of 6-32 screws, nuts, and brass sleeves, with two oil dots protecting the frame threads, provided hand grips while I wiped it down with denatured alcohol and coated it with XTC-3D epoxy:
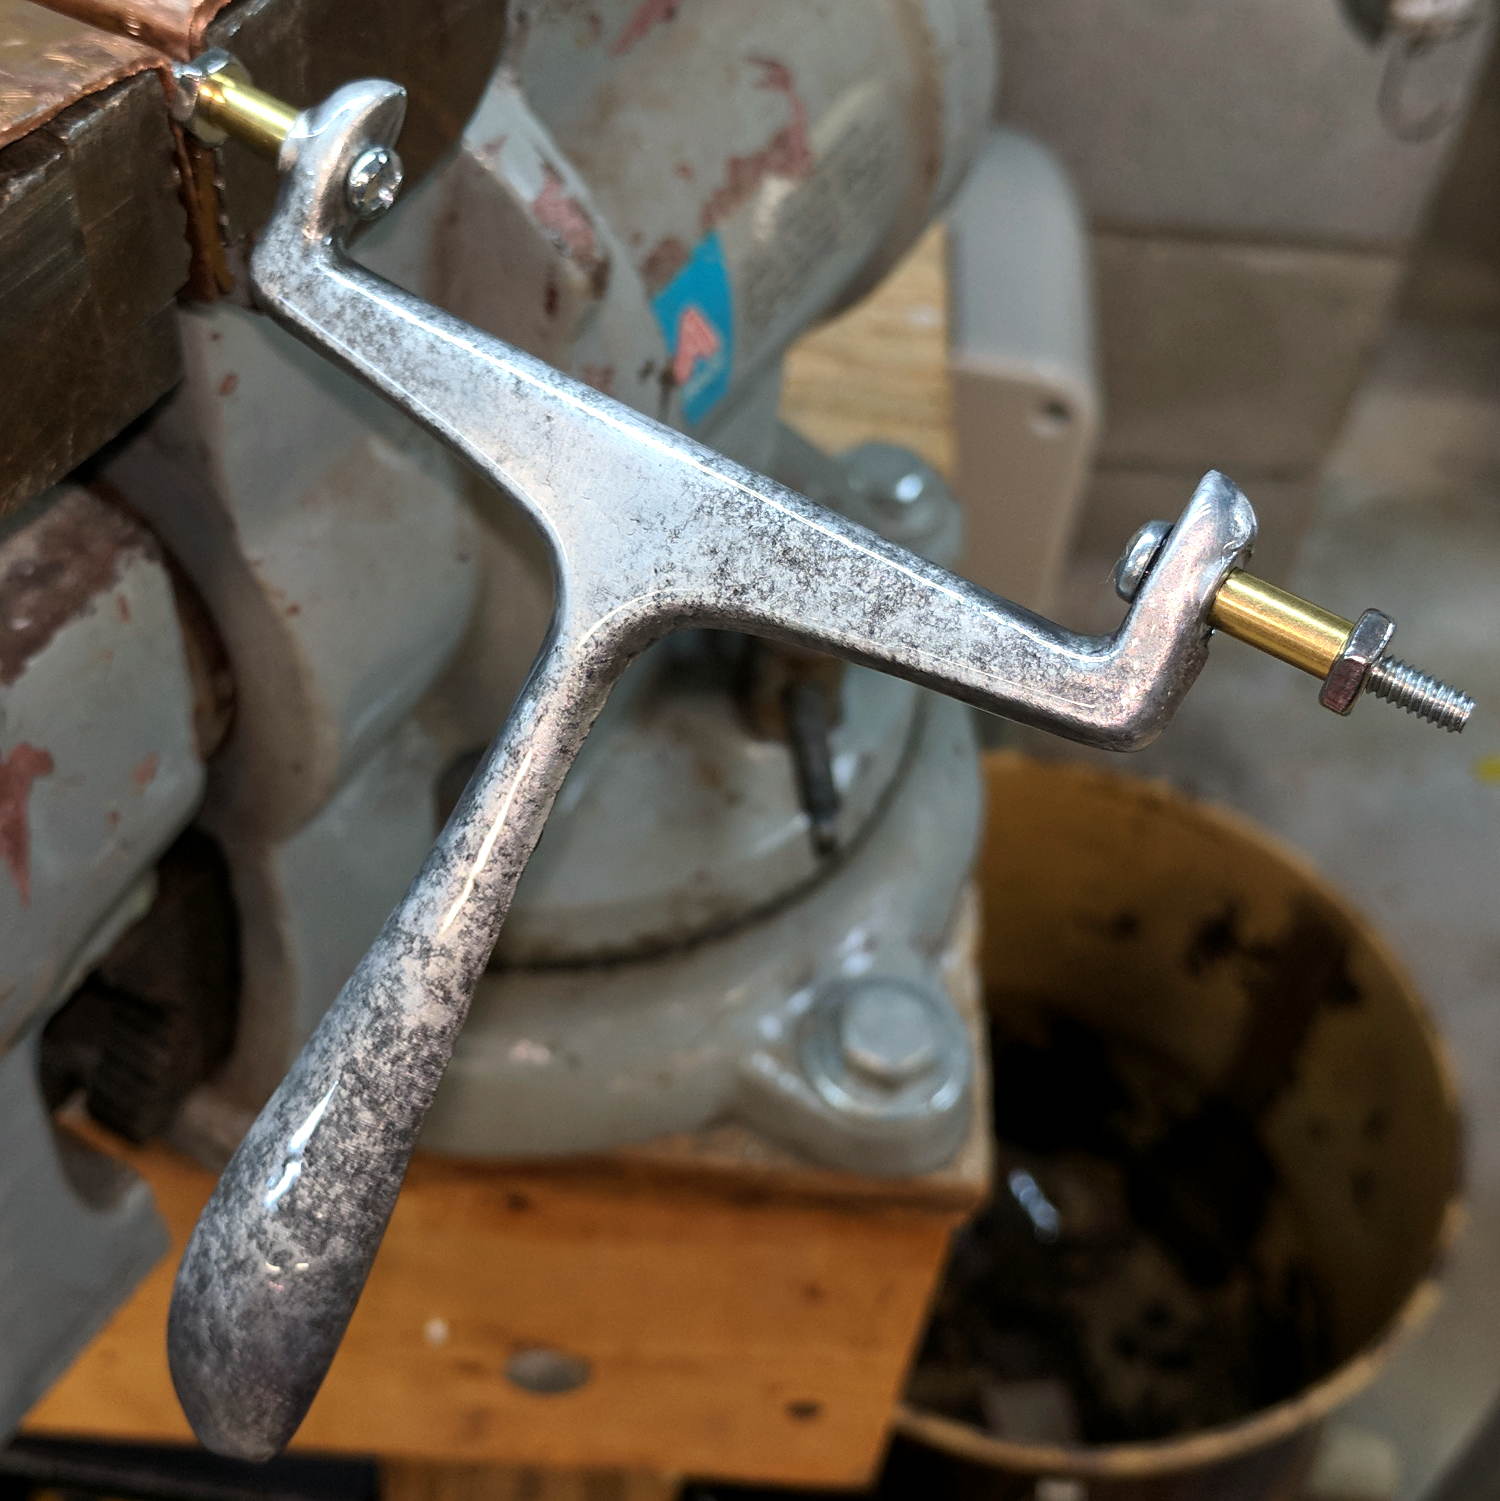
Turns out the mixing stick worked quite well to cover the entire thing, as the epoxy does a great job of leveling itself. I suppose wasting a tiny brush would be more professional, but …
It quietly dripped excess epoxy into a strategically placed trash can for about ten minutes. I wiped off the final drip before the epoxy solidified, leaving a smooth layer over the end of the handle:
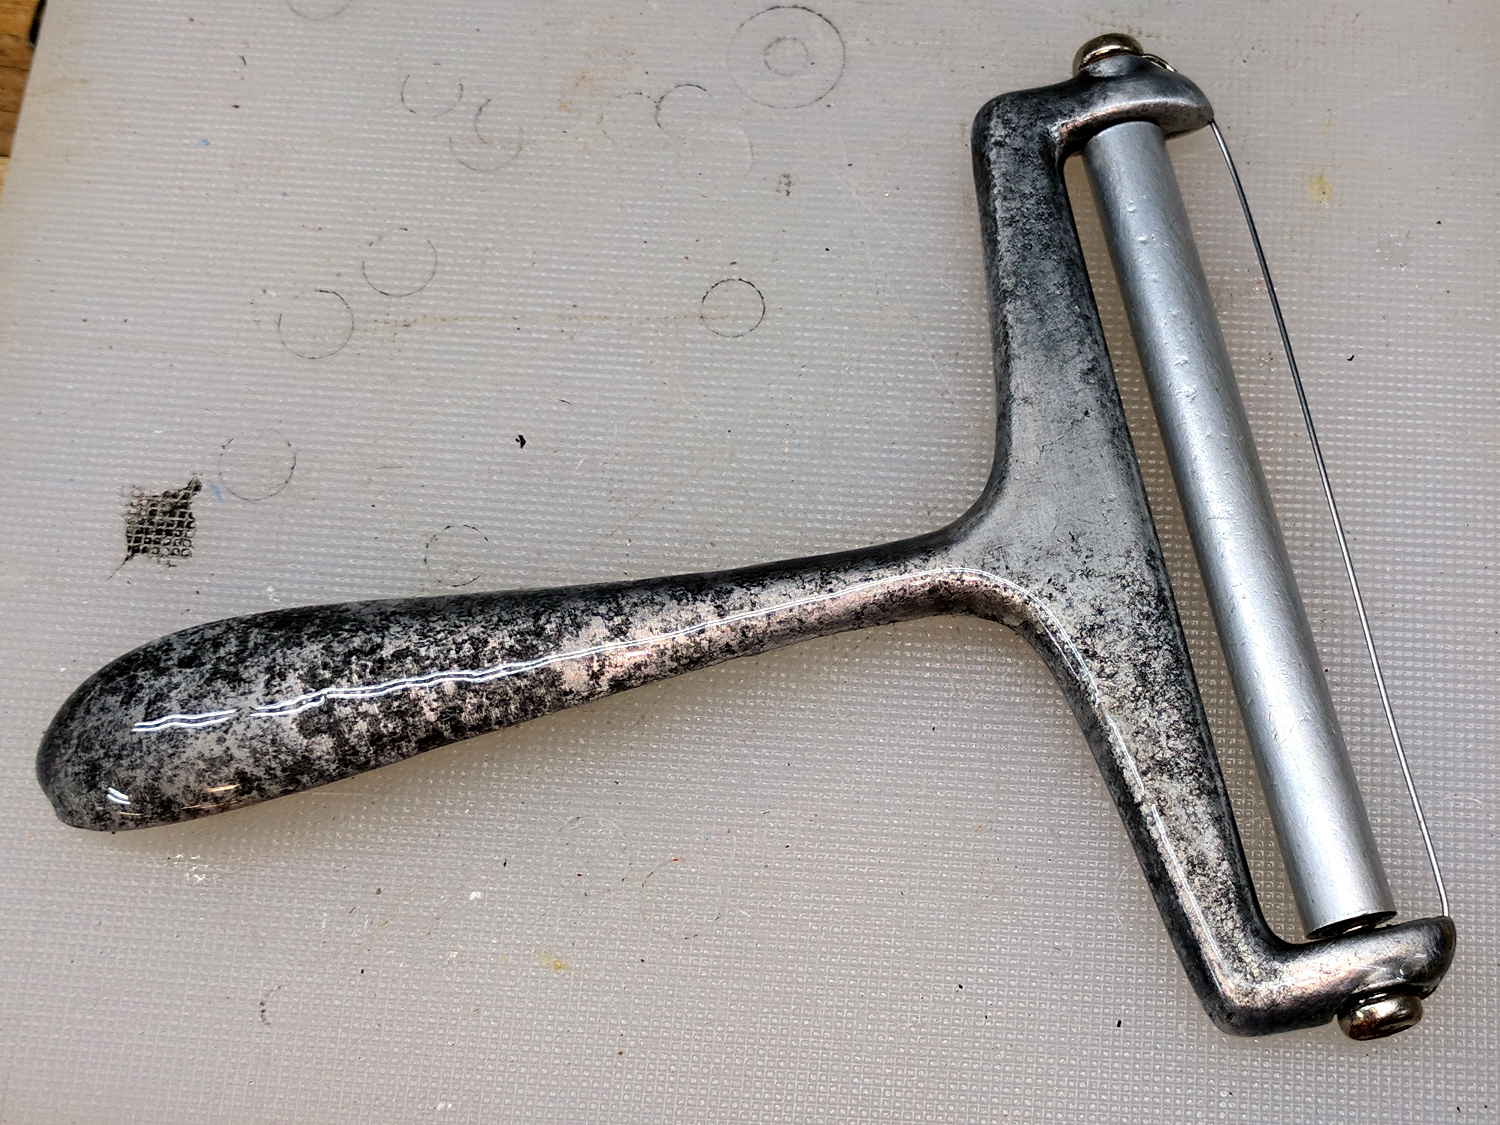
It’s back in service and works as well as ever, with a handle now smooth to the touch. I suppose I could have tinted the epoxy to hide the metal, but we regard those corrosion pits as beausage.
I’ve slathered XTC-3D on some 3D printed parts, but have no idea how durable it is; this should serve as an accelerated survival test under rather harsh usage.
The instruction sheet says XTC-3D isn’t the most transparent epoxy they make and, indeed, the layer left in the mixing pan came out more hazy than I expected:
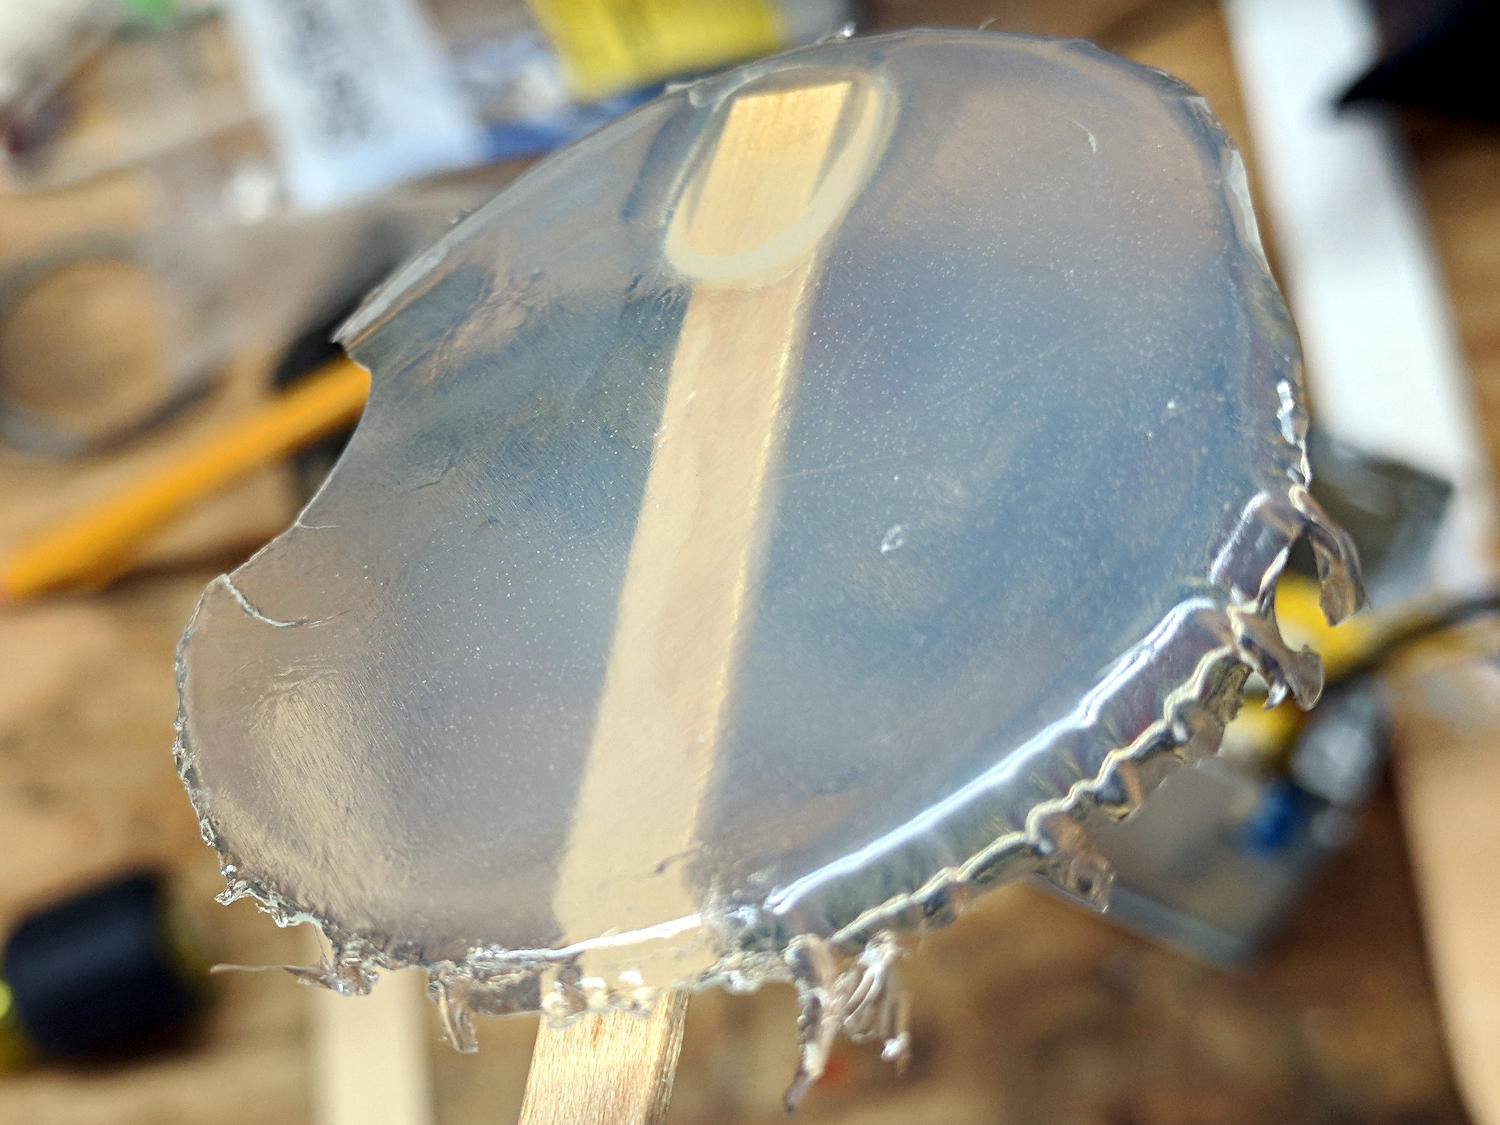
They point out the haze doesn’t matter for thin surface coatings, which is certainly true.
Thirteen years after the original repair on the left side and eight years after I fixed the drawer slide on the right side, this happened:

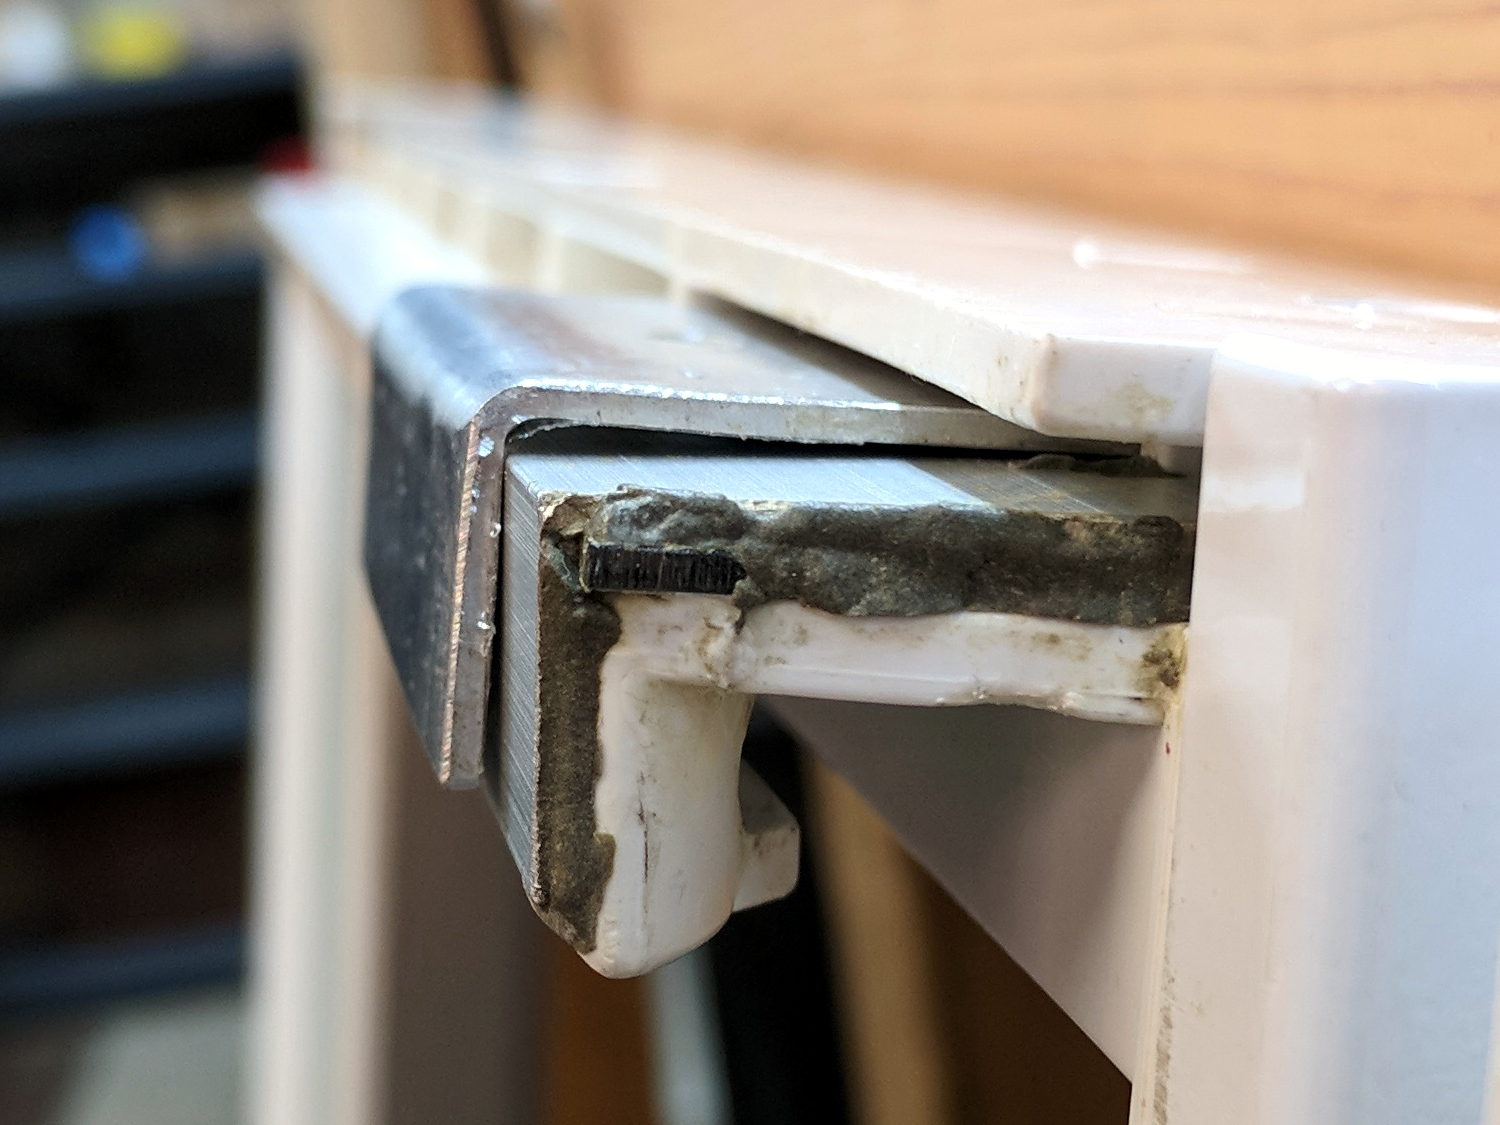
The general idea is to wrap a new bracket around the old bracket, because trying to remove the old one will probably cause more damage:
A pair of screws hold the new bracket to the shelf support:
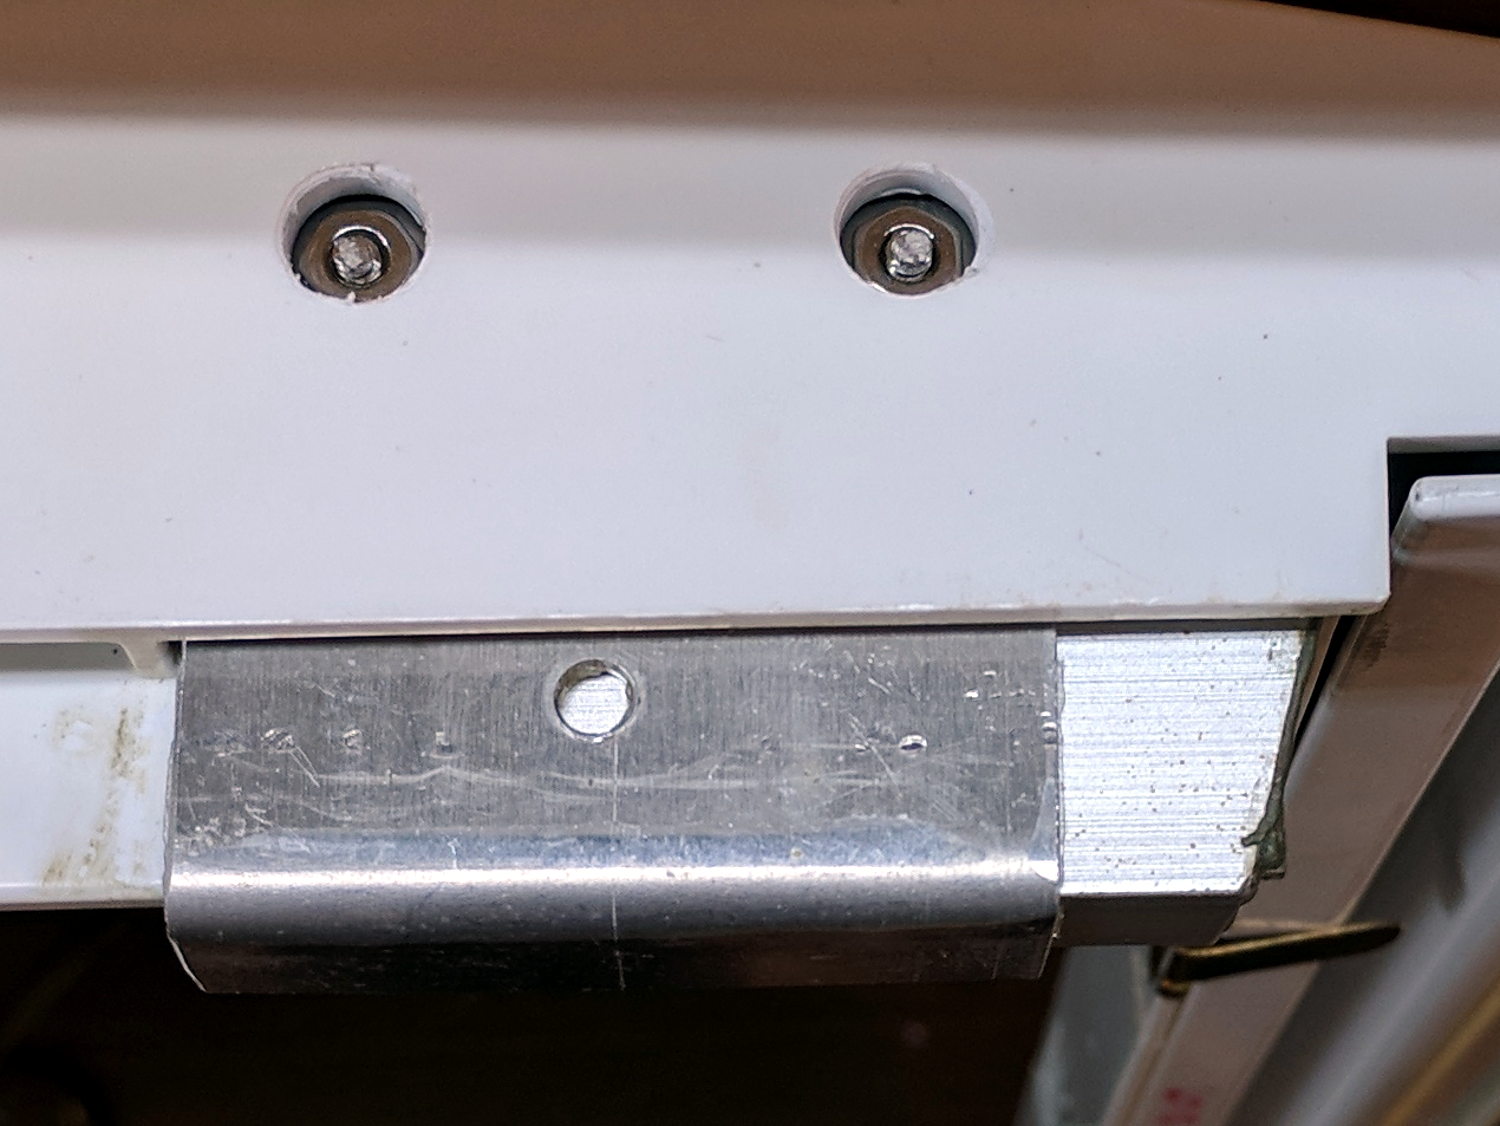
Those two screws must support the entire weight of the drawer, which is exactly what broke the original all-plastic frame and slide.
The epoxy chip and transparent plastic sheet in the first picture spaced the old aluminum bracket away from the shelf support and reduced the space beyond the new bracket enough to require drilling access holes. Fortunately, they’re hidden inside the support frame, so nobody will ever know.
The shelf support is a huge floppy rectangle, so I clamped it to the bench vise while drilling the holes:

The new bracket is on the right, with a sheet of white acrylic spacing it away from the shelf support by exactly the same distance as the angled aluminum snippet replacing the failed epoxy & plastic on the broken part:

The two holes in the middle of the aluminum parts show that I used exactly the same angle brackets as raw material. It’ll be a sad day when I eventually use the last of those brackets.
Putting the parts together, with double-stick tape holding all the parts in place, shows how they fit:
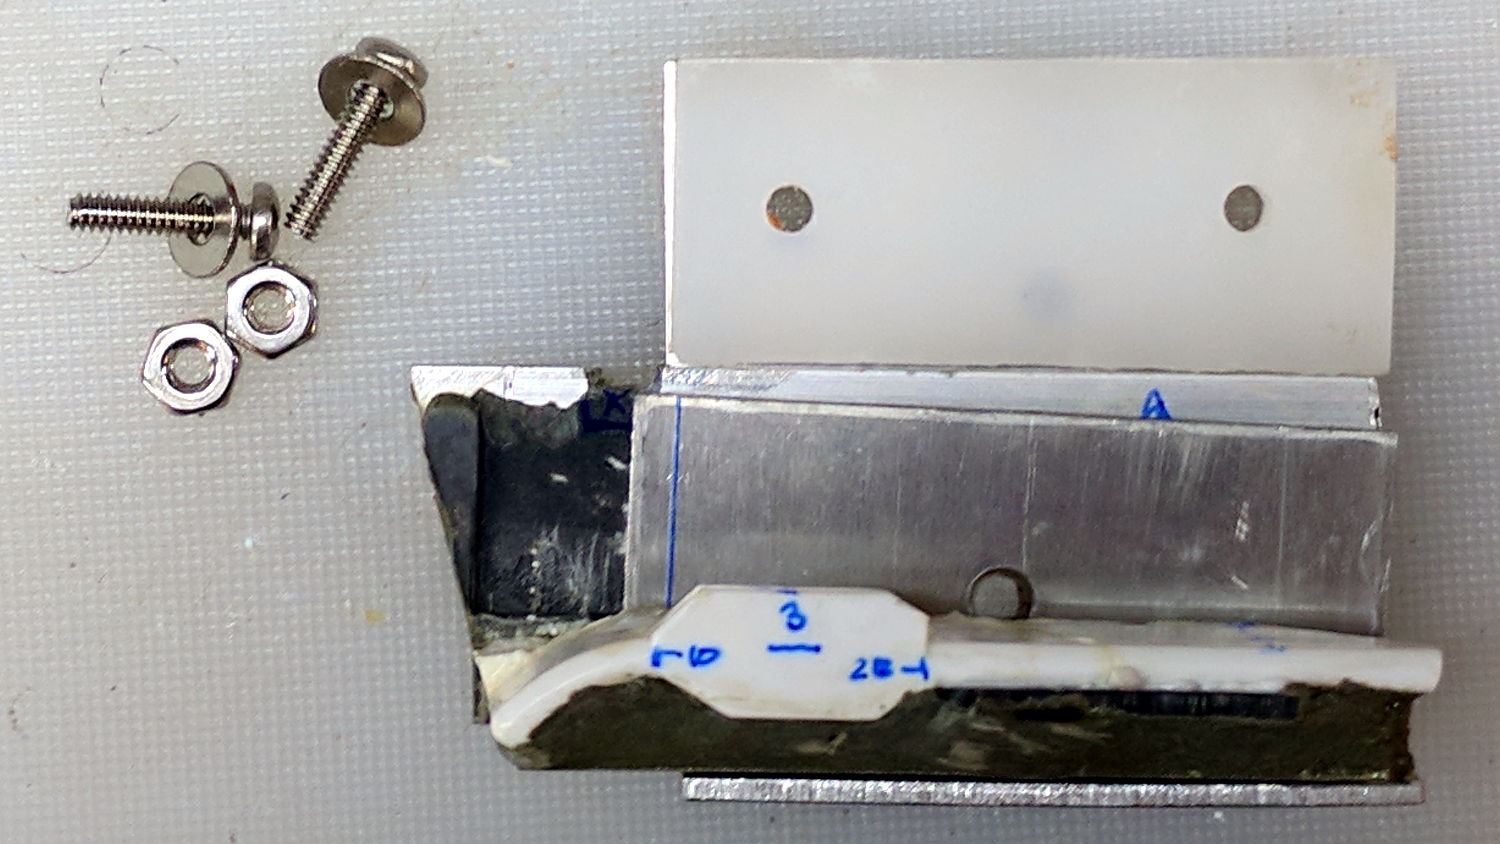
And then it just snapped into place. I didn’t bother pretending solvent glue would help anything, nor did I apply any epoxy, so this whole thing hangs from those two 4-40 screws. On the other paw, their steel beats the original white plastic.
I devoutly hope to never rebuild the actual drawer slide, but these dimensions may help somebody else out of a jam:

The vertical “40” dimension refers to the available space from the bottom of the white plastic part to the top of the shelf support frame; the new bracket is a tad shorter than that.
The plastic parts in that refrigerator have been a complete disappointment: were it not for my relentless repair jones, we’d likely be on our third or fourth refrigerator by now. Oddly, the cooling parts continue to chug along (*), without more than the occasional loud noise in the middle of the night.
We’re definitely doing our part to reduce our waste stream.
(*) The most recent freezer fan hasn’t failed yet!
The LT1920 instrumentation amplifier now sports two silver-mica caps on its inputs as a differential-mode input filter cutting back strong RF signals (clicky for more dots):
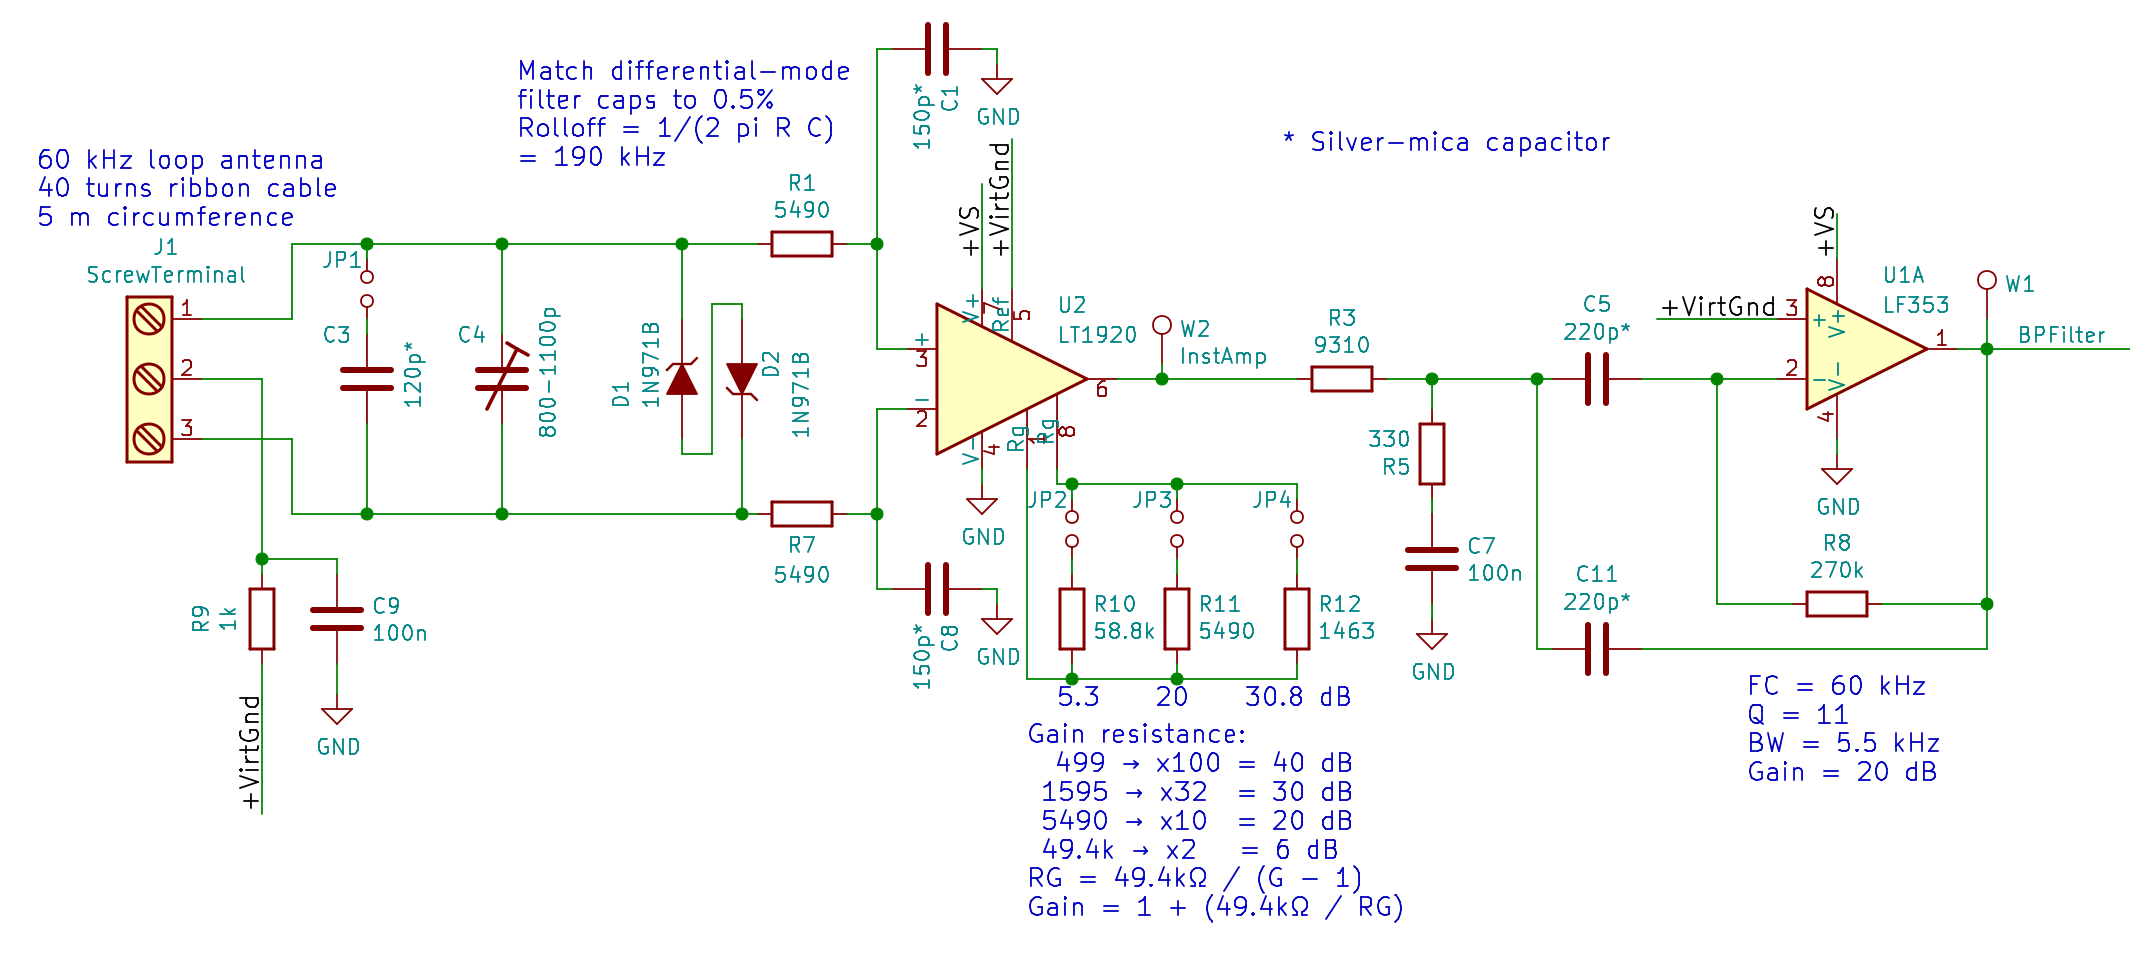
In principle, a DM filter should eliminate RF rectification from out-of-band signals, although I think the attic is quiet enough to not need any help. The caps form a simple RC LP filter rolling off at 5.490 kΩ × 150 pF → 193 kHz, high enough above the 60 kHz signal to not make much difference down there.
The silver-mica caps come from the Big Box o’ Caps, which contained an envelope with a few large 150 pF ±1% caps and a bag stuffed with similar 147 pF ±1% caps. Mixed in with the latter were some smaller 147 pF caps (*) of no particular tolerance (perhaps 5%), from which I neurotically matched a pair to 0.05 pF without too much effort. Doesn’t matter, given the other tolerances and suchlike, but it was amusing.
I’d inadvertently grounded the cold end of the 330 Ω input resistor in the LM353 bandpass filter, now properly tied at the Vcc/2 virtual ground to take the DC load off the LT1920 output: a 100 nF cap (27 Ω at 60 kHz) stores the bias level without messing up the filter shape.
A similar cap rebiases the protected resonator at the LT1010 buffer input:
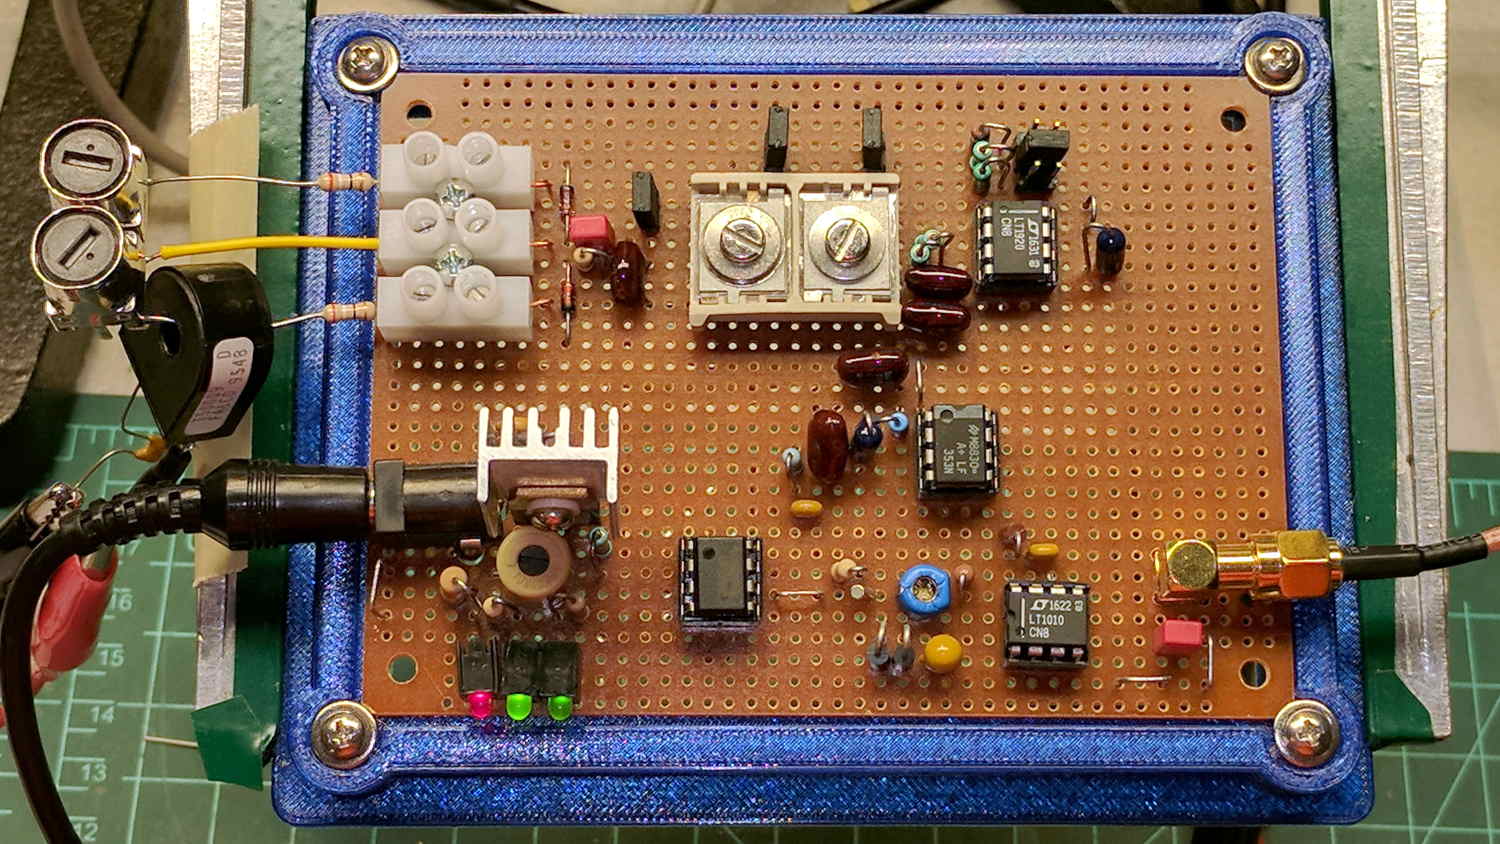
The new caps aren’t all that visible and the resonator vanishes in the clutter:
Next: find out how well it works!
(*) Yes, there were two envelopes between 150 pF and 147 pF:

I eventually noticed the yellow LED indicating +24 V input from the power supply (previously, a noisy wall wart) was dark. Poking around revealed I’d inadvertently installed a 1 kΩ ballast resistor:
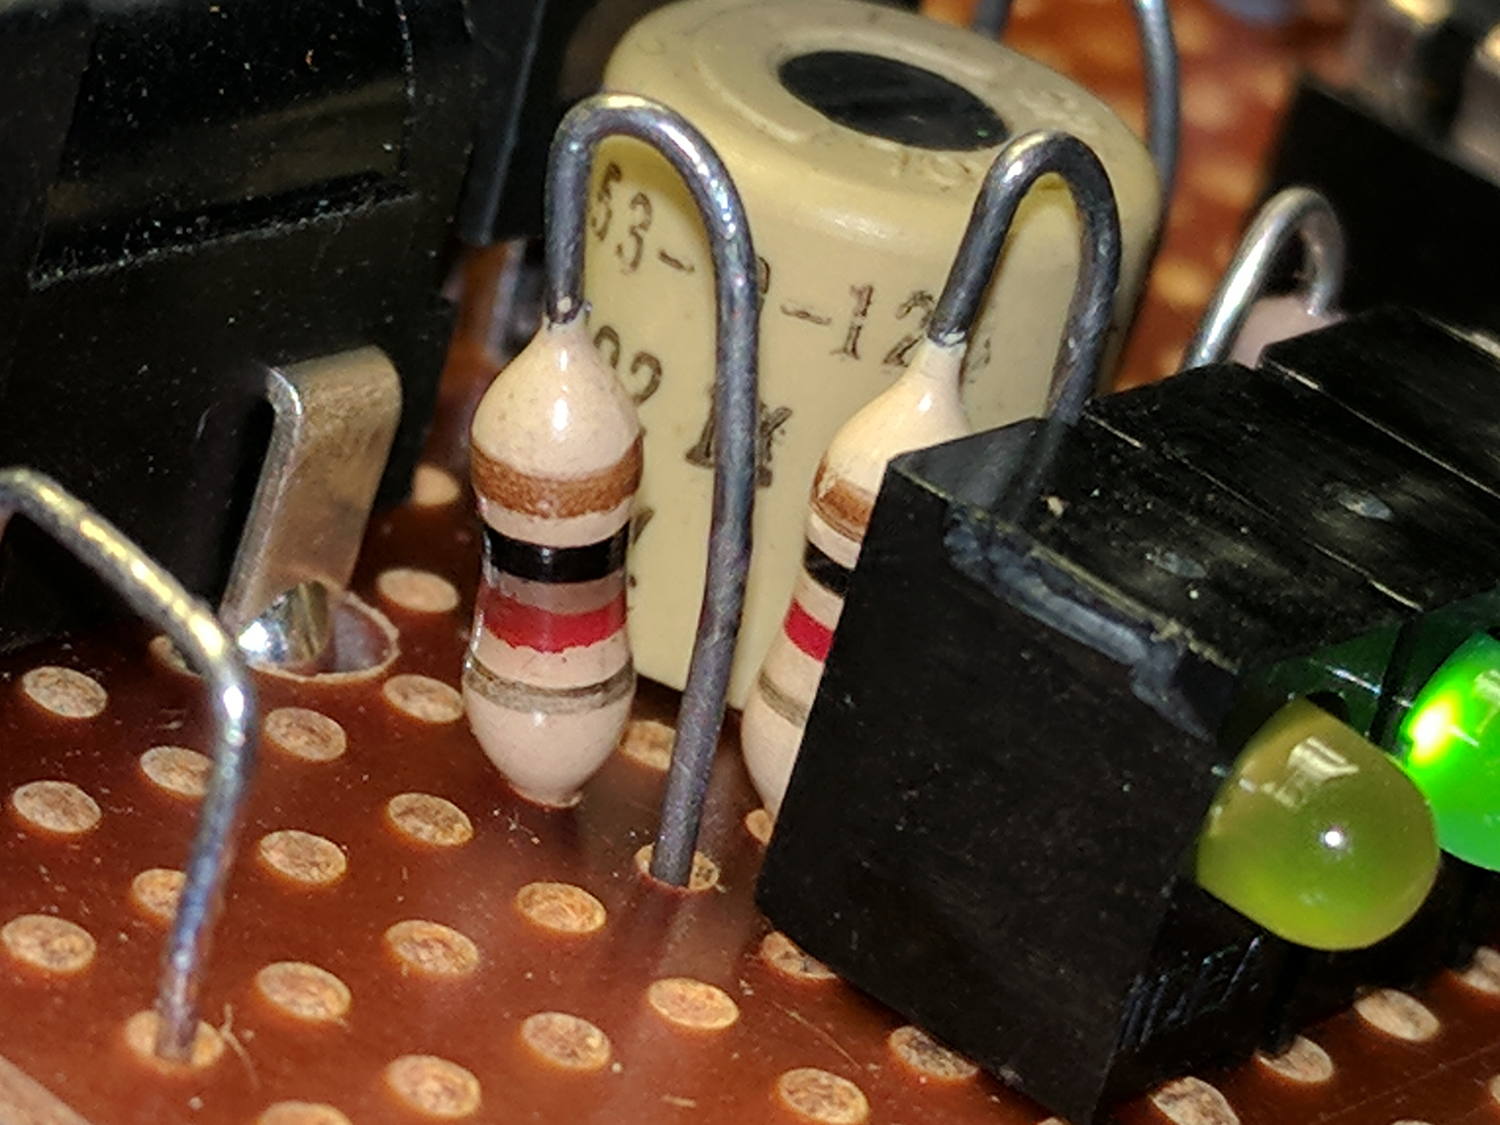
A 1/4 W resistor can’t dissipate half a watt for very long, as shown by the discolored circuit board around the leads and the faint smell of electrical death in the area.
I swapped in a 3.3 kΩ resistor, the yellow LED lit up for a few seconds, then went dark again. This time, the LED was dead; apparently, it’d been overstressed for long enough to fail. I can’t be too annoyed.
Unfortunately, replacing the LED required removing the entire housing with all three LEDs, chopping off the defunct block, reinstalling the attenuated block with the two green LEDs, installing a similar red LED, and finally installing a nice 3.3 kΩ half-watt resistor:
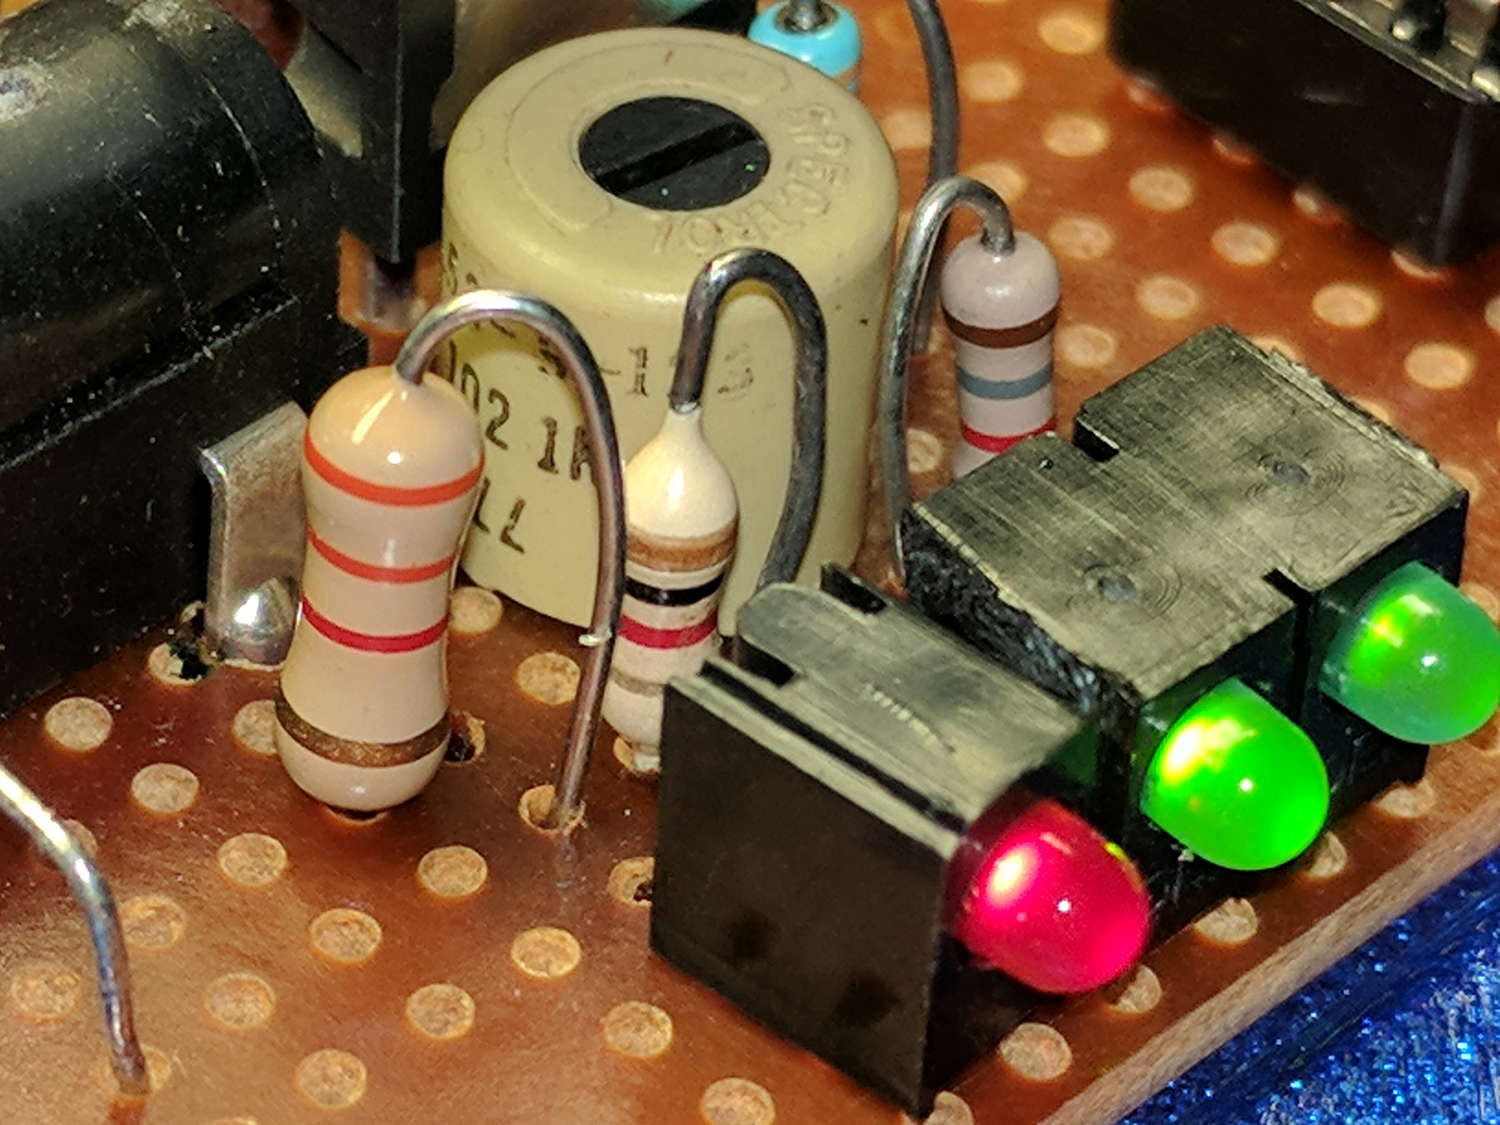
So it goes …
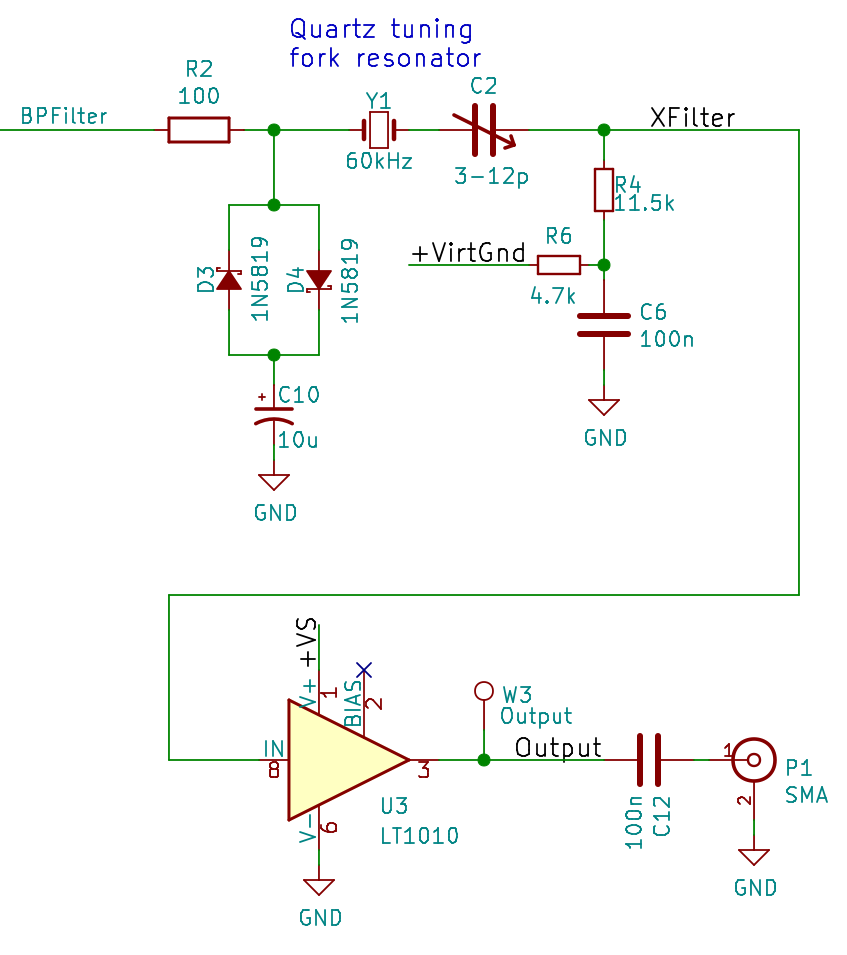
Limiting the resonator drive to about 1 μW in the face of wildly varying RF from the antenna (or the occasional finger fumble) requires brute force. A nose-to-tail pair of Schottky diodes seems to do the trick:
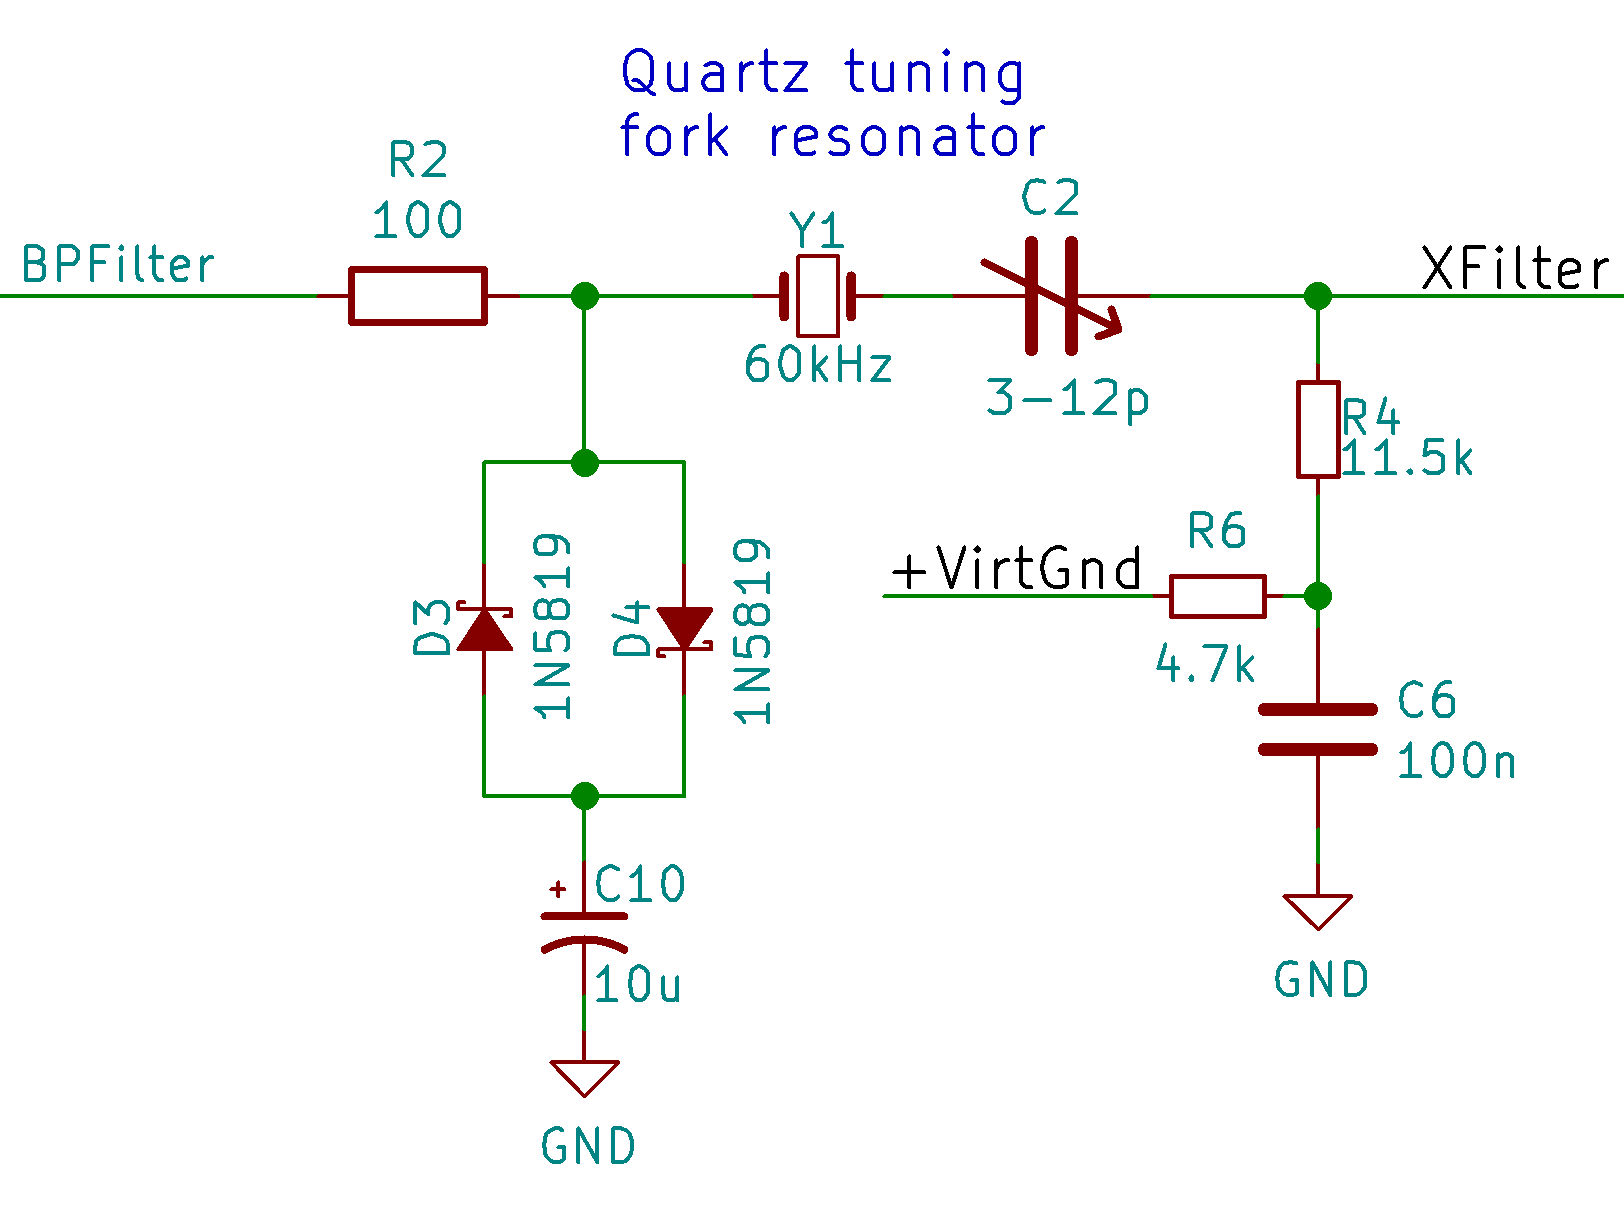
The 100 Ω resistor blunts the drive from the LM353 op amp (implementing a bandpass filter) when the signal peaks exceed 200-ish mV in either direction from the Vcc/2 bias stored in the 10 μF cap.
The 11.5 kΩ resistor downstream of the resonator isolates it from the Vcc/2 bias, with the 100 nF cap sinkholing the signal and the 4.7 kΩ resistor preventing feedback into the bias supply. The cap looks like 26 Ω at 60 kHz, so the feedback runs -52 dB from the output and the bias supply knocks it down a bit more. The preceding amps apply 40-ish dB of gain from the antenna terminals, so the loop gain looks OK.
It’s another few components on the board:
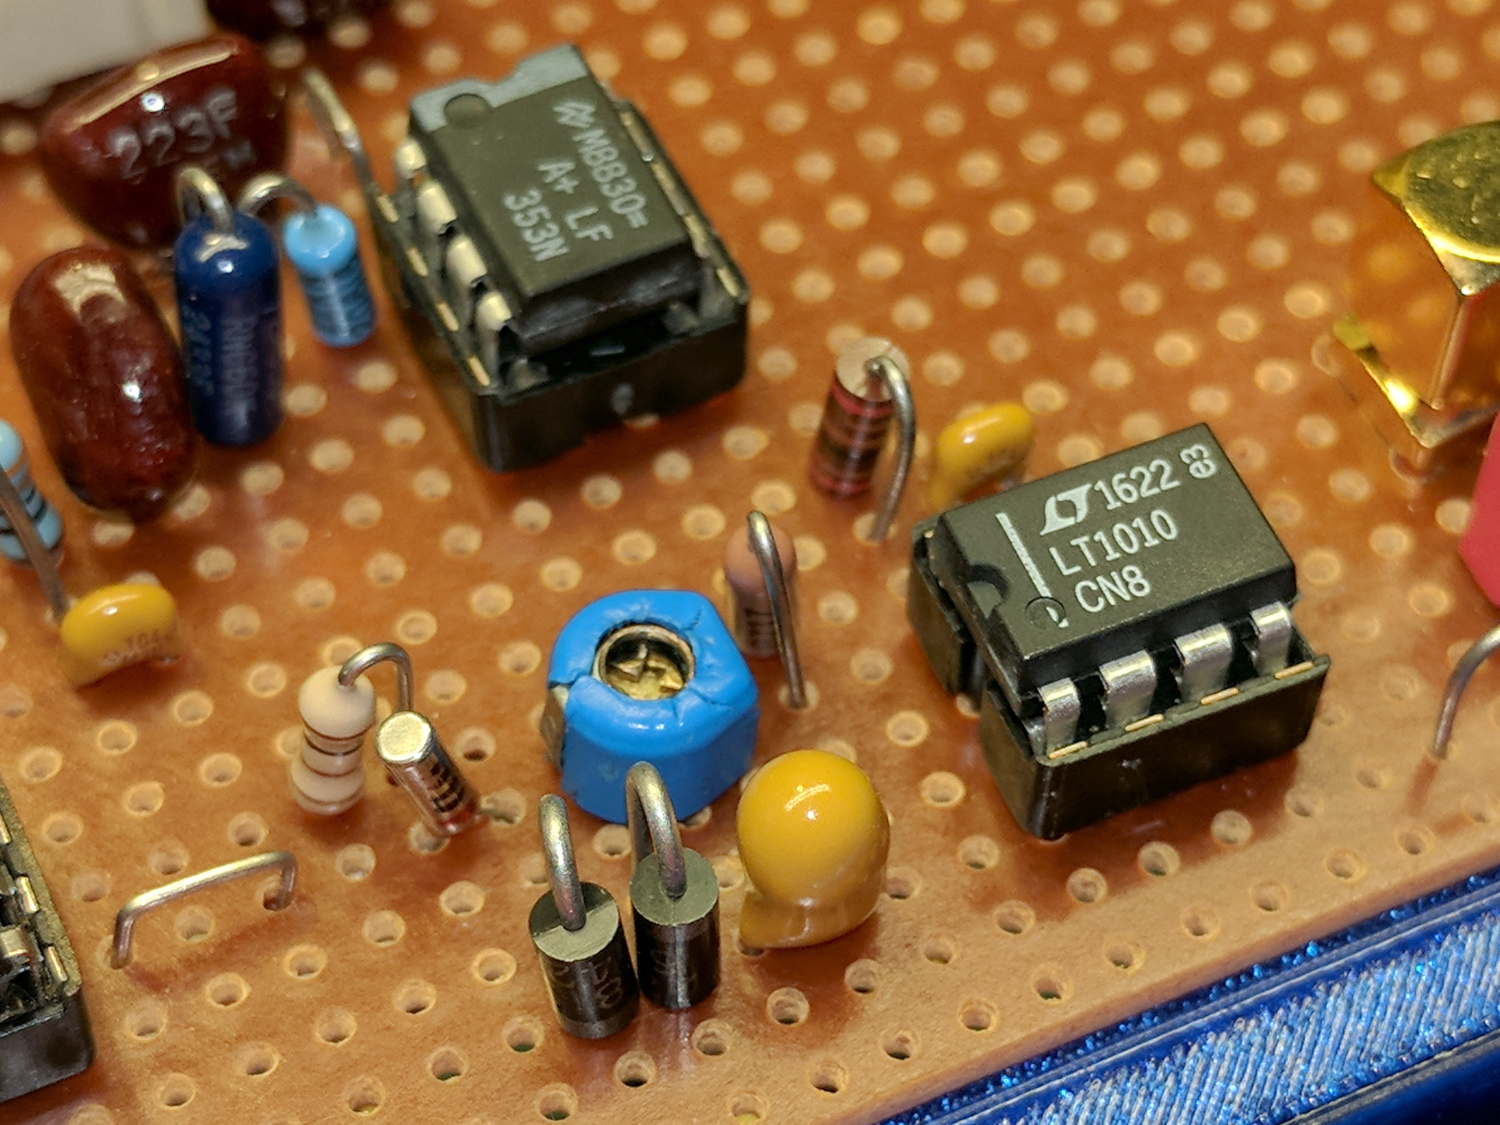
The blue twiddlecap should allow pulling the tuning fork’s series resonance upward to exactly 60 kHz.
Applying way too much signal to the antenna terminals in order to get 1 Vpp from the LM353 shows the limiter in action:
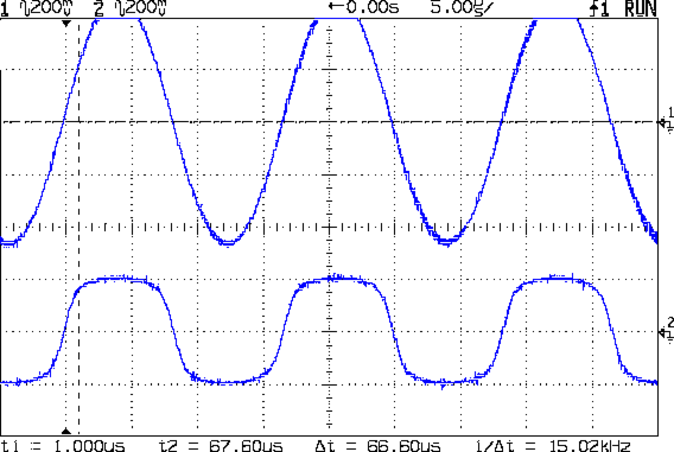
The resonator sees no more than 200 mV in either direction from the bias level, so it’s all good.
On the low end, the diodes have no effect:
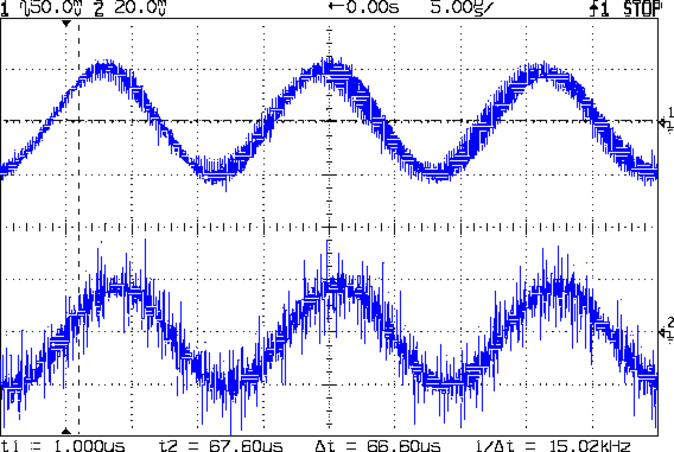
Pay no attention to all that noise.
My first thought was to put the diodes across the resonator, a Bad Idea: straight up, doesn’t work. The 1N5819 datasheet shows they have about 300 pF of junction capacitance at zero bias and a pair of ’em will swamp the resonator’s internal 0.8 pF parallel capacitance and punch it out of the circuit.
The headset on my Tour Easy ‘bent worked its way loose, which led to a disturbing discovery: the headset wrench I made from a discarded flat wrench vanished with the shop tools donated to MakerSmiths.
Fortunately, we live in the future:
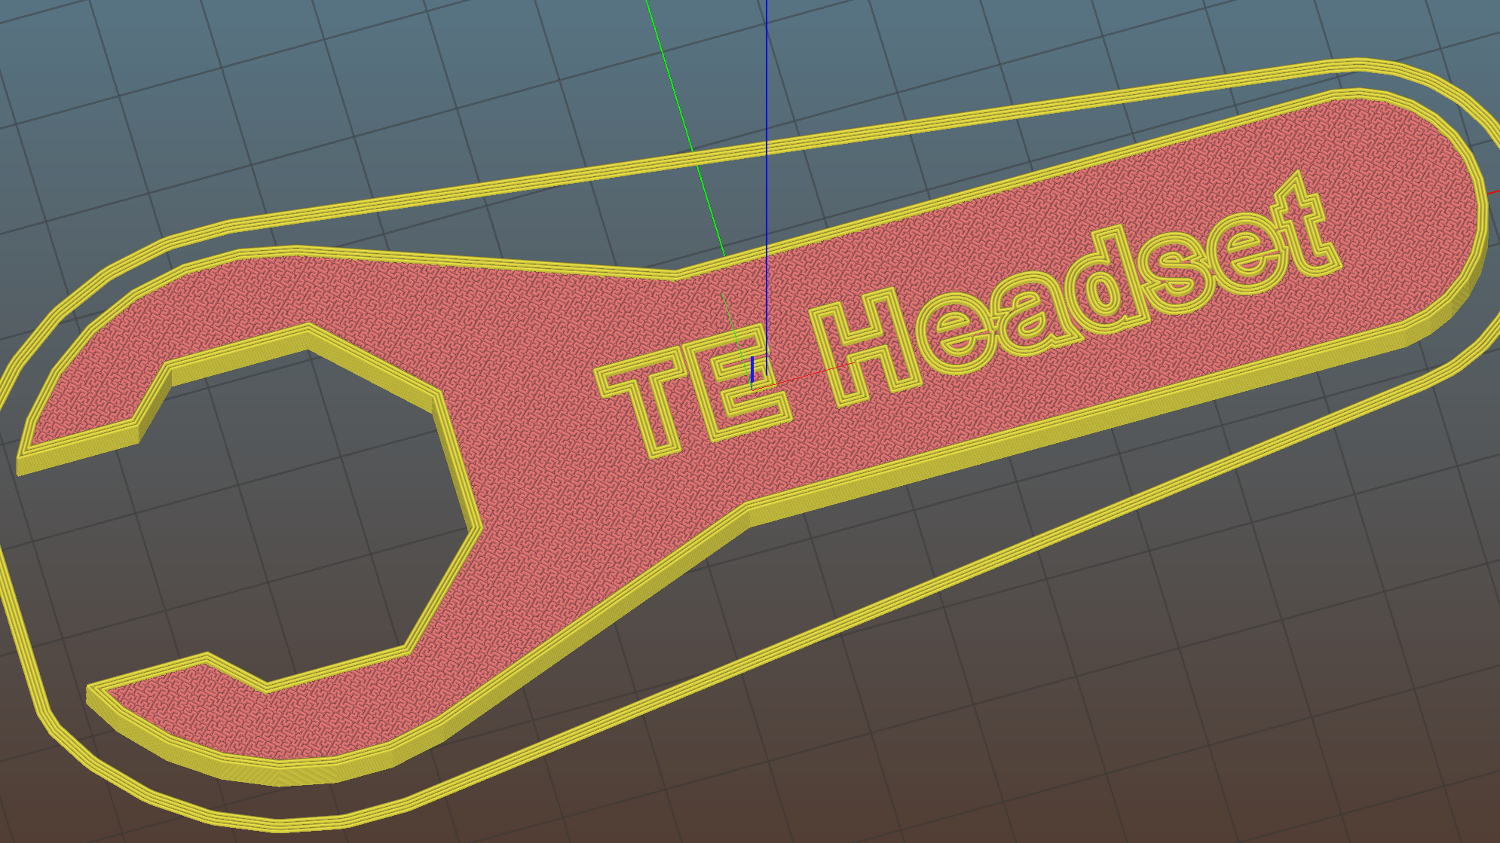
A thin plastic wrench is absolutely no good for torquing down the locknut, but that’s not what it’s for. Adjust the bearing race to the proper preload with this wrench, hold it in place, then torque the locknut with the BFW.
The OpenSCAD source code as a GitHub Gist:
| // Tour Easy Headset Wrench | |
| // Ed Nisley KE4ZNU – September 2017 | |
| /* [Extrusion] */ | |
| ThreadThick = 0.25; // [0.20, 0.25] | |
| ThreadWidth = 0.40; // [0.40] | |
| function IntegerMultiple(Size,Unit) = Unit * ceil(Size / Unit); | |
| Protrusion = 0.01; // [0.01, 0.1] | |
| HoleWindage = 0.2; | |
| //- Sizes | |
| /* [Dimensions] */ | |
| WrenchSize = 32.0; // headset race across-the-flats size | |
| NumFlats = 8; | |
| JawWidth = 10.0; | |
| JawOD = 2*JawWidth + WrenchSize; | |
| echo(str("Jaw OD: ",JawOD)); | |
| StemOD = 23.0; | |
| WrenchThick = 5.0; | |
| HandleLength = 2*JawOD; | |
| HandleWidth = 25.0; | |
| //- Build things | |
| difference() { | |
| linear_extrude(height=WrenchThick,convexity=4) { | |
| hull() { // taper wrench body to handle | |
| circle(d=JawOD); | |
| translate([0.75*JawOD,0,0]) | |
| circle(d=HandleWidth); | |
| } | |
| hull() { // handle | |
| translate([0.75*JawOD,0,0]) | |
| circle(d=HandleWidth); | |
| translate([HandleLength,0,0]) | |
| circle(d=HandleWidth); | |
| } | |
| } | |
| translate([0,0,-Protrusion]) | |
| rotate(1*180/NumFlats) { // cosine converts across-flats to circle dia | |
| cylinder(d=WrenchSize/cos(180/NumFlats),h=(WrenchThick + 2*Protrusion),$fn=NumFlats); | |
| } | |
| translate([-StemOD,0,WrenchThick/2]) | |
| cube([2*StemOD,StemOD,(WrenchThick + 2*Protrusion)],center=true); | |
| translate([WrenchSize,0,WrenchThick – 3*ThreadThick]) | |
| linear_extrude(3*ThreadThick + Protrusion,convexity=10) | |
| text(text=str("TE Headset"),size=8,spacing=1.20,font="Arial",halign="left",valign="center"); | |
| } |
Now, I’d like to say that was easy, but in actual point of fact …
First, I forgot to divide by cos(180/6) to convert the across-the-flats size to the diameter of OpenSCAD’s circumscribed hexagon-as-circle, which made the wrench uselessly small:

If you have a 28 mm nut with low torque requirements, though, I’ve got your back.
While I had the hood up, I slenderized the handle into a much shapelier figure:
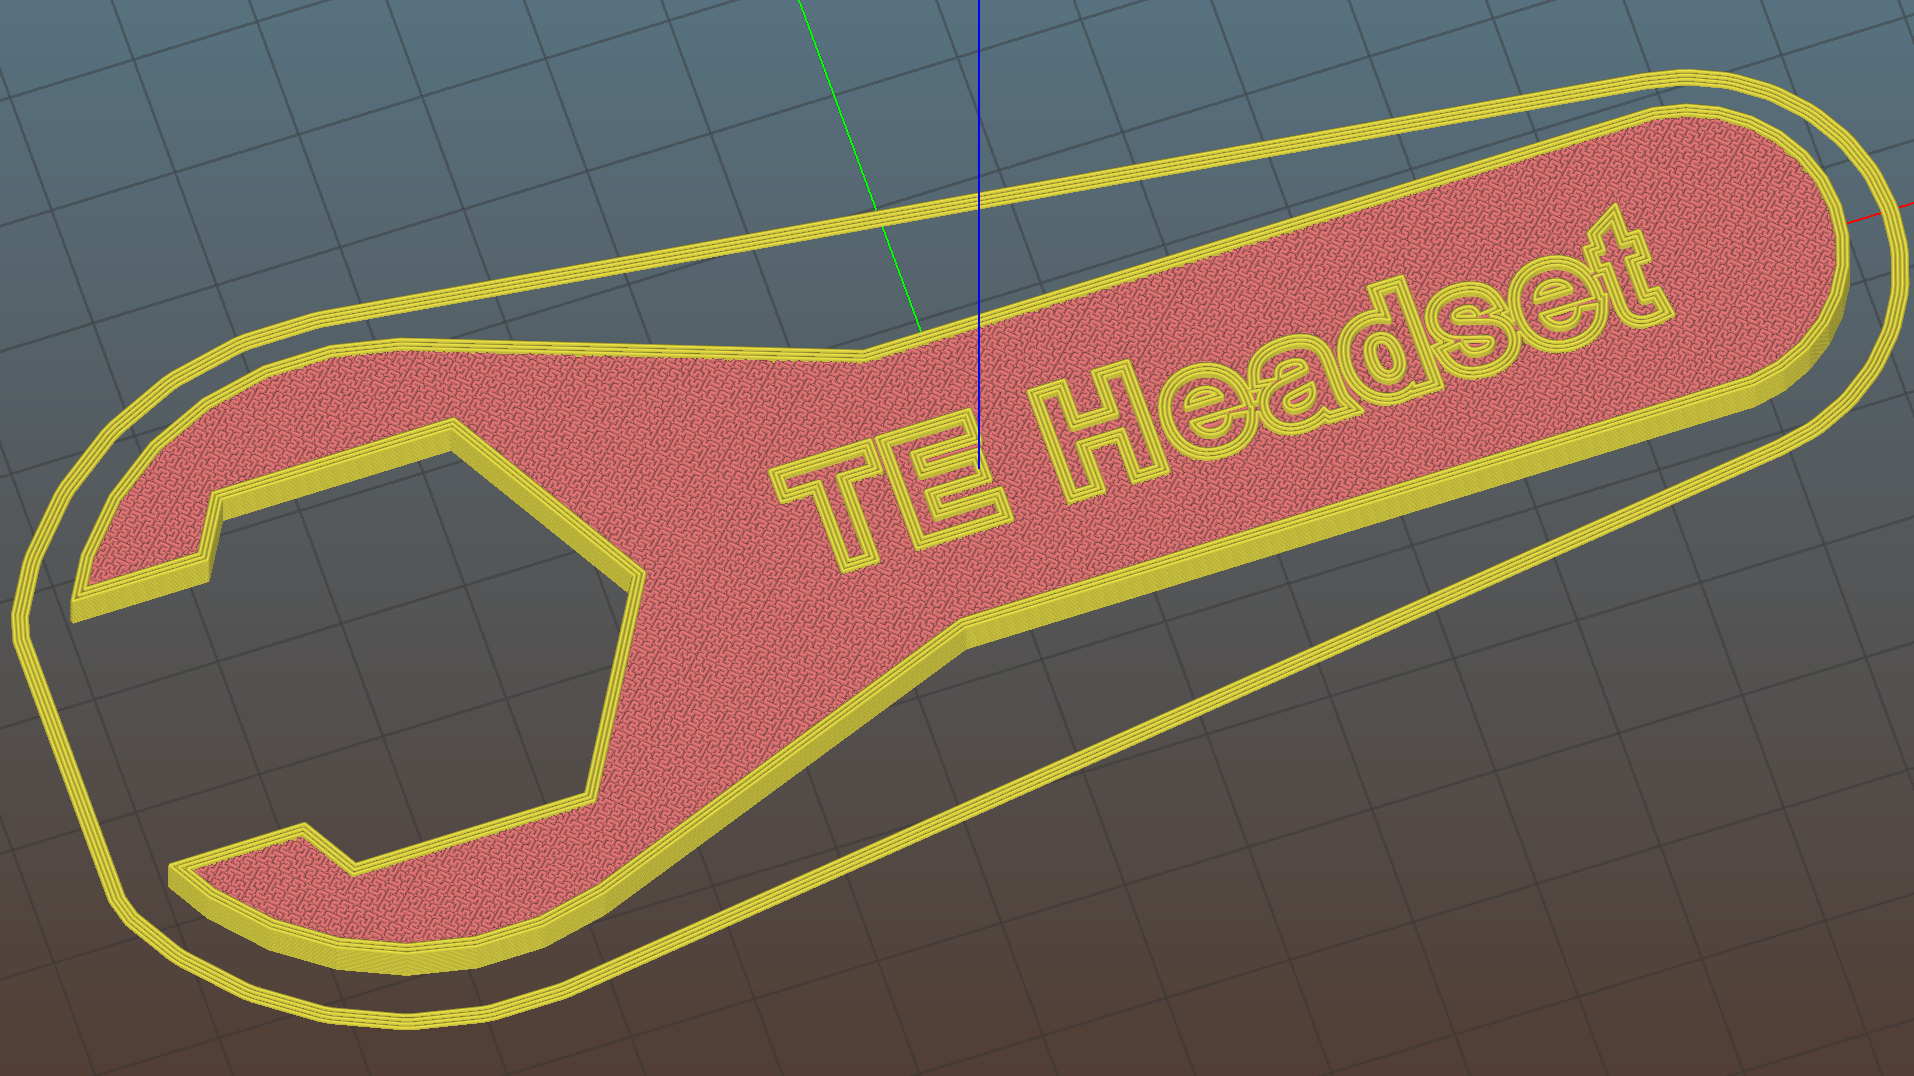
Trotting off to the garage with a warm plastic wrench in hand, I discovered the blindingly obvious fact that the headset nuts have eight sides. On the upside, the number of sides became a parameter, so, should you happen to need a five-sided wrench (perhaps on Mars), you can have one.
So, yeah, it’s rapid prototyping in full effect:
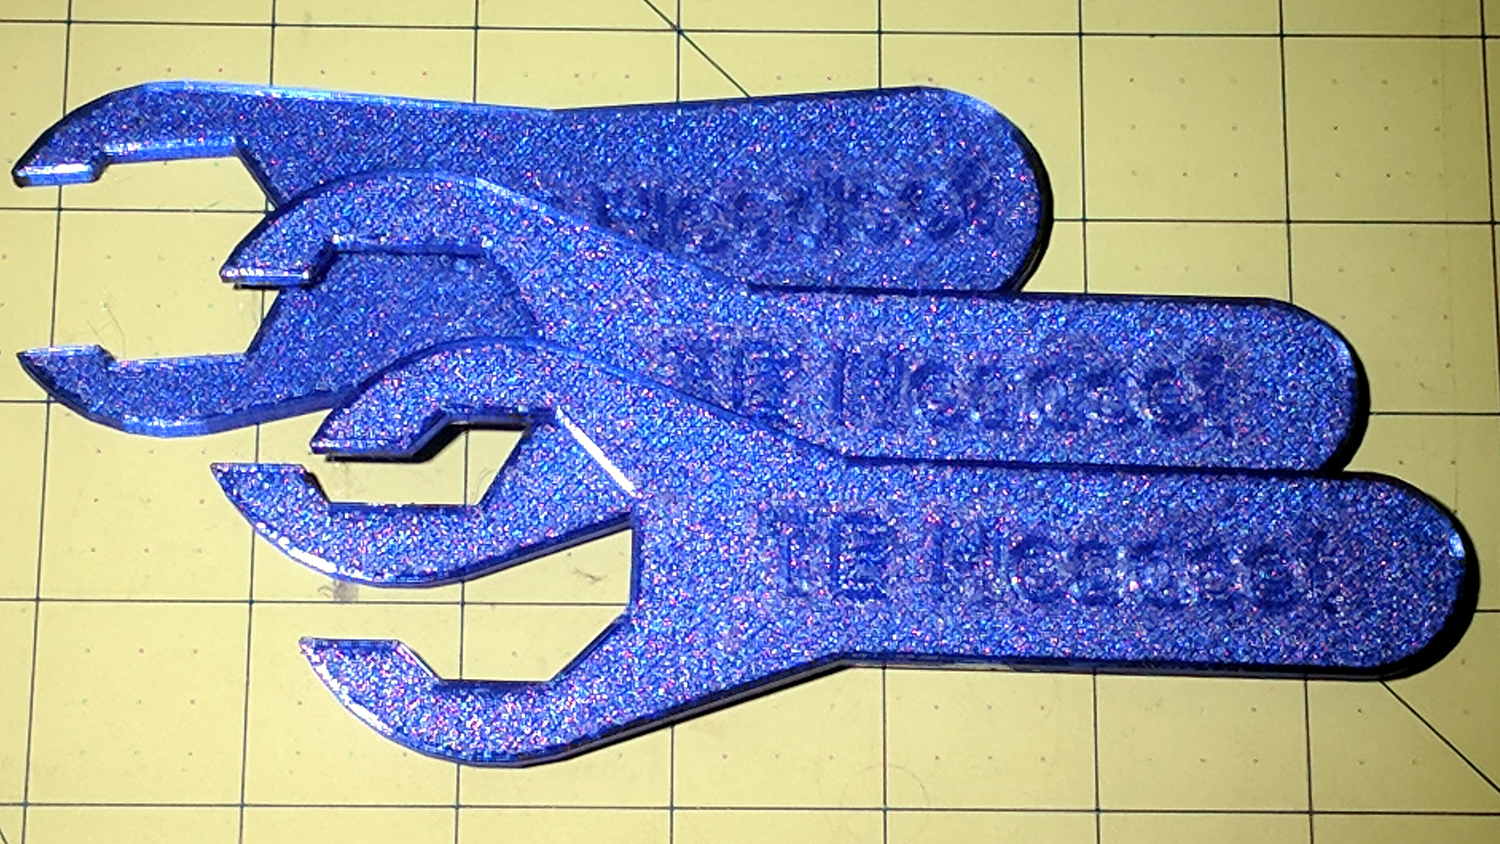
Remember, kids, never design while distracted …

