-
Makergear M2: Cushwa Owl
You’ve seen the overview pictures of the half-scale cushwa Owl earlier, so here are some details…
The front view:
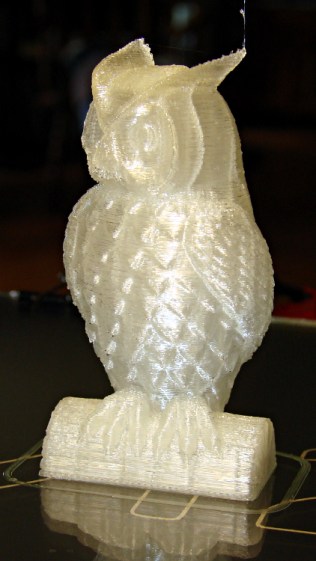
M2 – cushwa Owl – half scale The left side view:
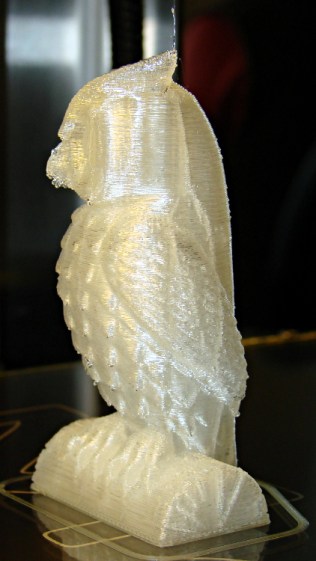
Owl – half size – left The conspicuous vertical lines come from the 0.10 infill honeycomb; there are no visible retraction zippers and the surface is smooth to the touch.
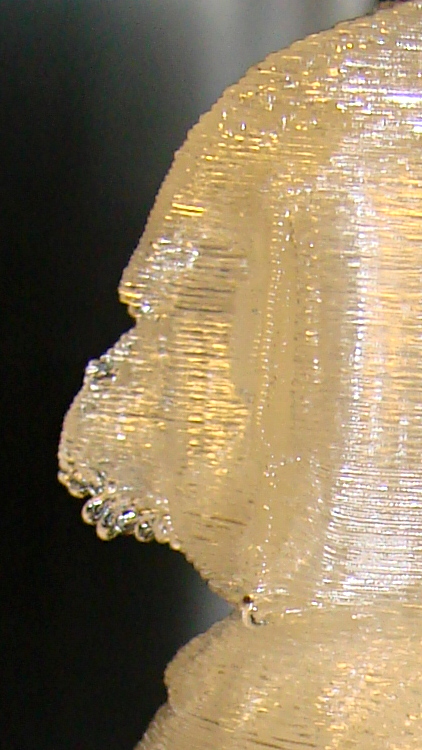
A closeup of the beak shows the crystal-clear drooping filament; a similar effect happened on the downward-pointing feather tips. Generally, this is a sign of too-hot extrusion, but at 165 °C I’m not convinced that’s applicable. It may simply be too much overhang at this scale:
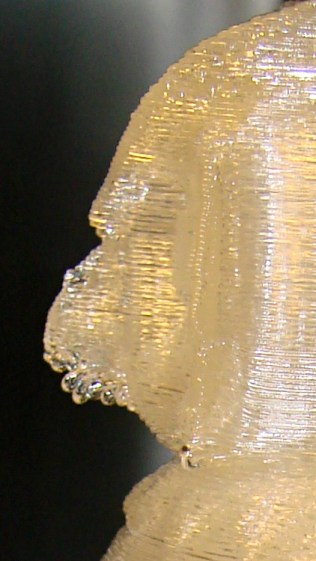
M2 – cushwa Owl – beak detail Overall, it’s pretty good. The config info doesn’t include the external perimeter speed, which I’ve been dialing back from an insanely high value. I think it was 75 for this one, which might be flinging the filament off the edge of the beak below that steep overhang.
The slic3r configuration:
; generated by Slic3r 0.9.8 on 2013-03-28 at 10:28:53

; layer_height = 0.25
; perimeters = 1
; top_solid_layers = 3
; bottom_solid_layers = 3
; fill_density = 0.10
; perimeter_speed = 100
; infill_speed = 300
; travel_speed = 500
; scale = 1
; nozzle_diameter = 0.35
; filament_diameter = 1.70
; extrusion_multiplier = 0.9
; perimeters extrusion width = 0.40mm
; infill extrusion width = 0.40mm
; first layer extrusion width = 0.39mm
No source code, as it’s directly from the STL on Thingiverse.

-
Subscribe
Subscribed
Have a WordPress.com account? Log in now.

