Ed Nisley's Blog: Shop notes, electronics, firmware, machinery, 3D printing, laser cuttery, and curiosities. Contents: 100% human thinking, 0% AI slop.
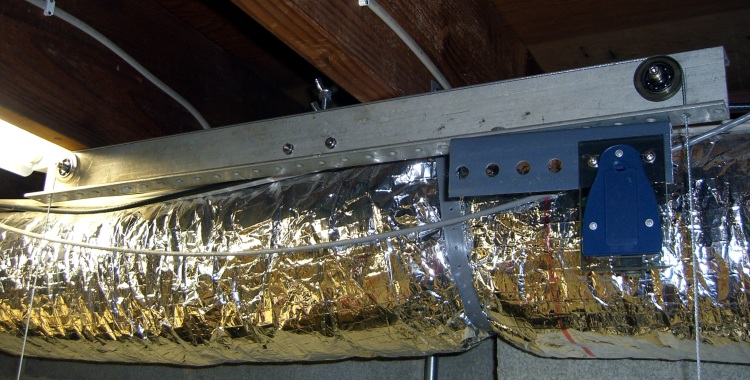
I’d planned to whack the ends off the counterweight gantry I made for Cabin Fever Expo and mount them to a plywood plate, but I hate cutting stuff up. Turns out that the entire beam fit very nicely on the floor joists over the mill and the counterweight even hangs in a reasonable location.
Sherline counterweight gantry on ceiling
I used a plumb bob to get the pulley pretty close to the right location, then simply moved the beam around until the cable hung down through the middle of the hole. Securing it to two joists means it’s pretty nearly perfectly level along both axes, so the cable’s close enough to being vertical.
Of course, holding it overhead, aligning it, and then drilling the holes in the joists required three or four hands.
The blue doodad on the right end is the laser aligner on its new bracket. The crinkly silver tube is an exhaust duct for the never-sufficiently-to-be-damned radon mitigation air exchanger, a topic I refuse to discuss.
The observant reader will note that I still haven’t made dust shields for those open ball bearings.
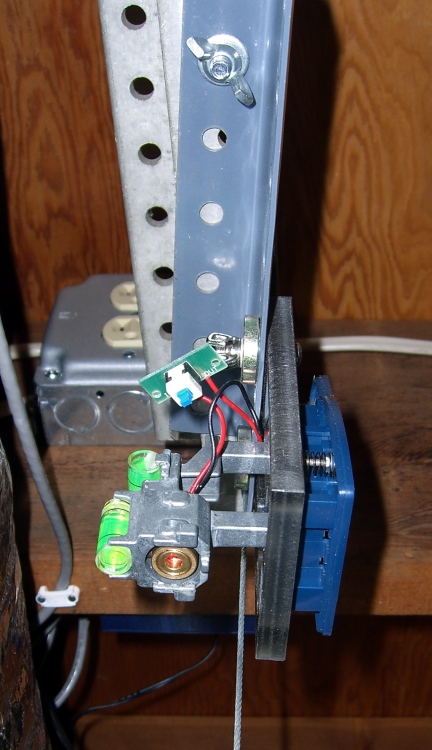
I mentioned my cheap laser alignment gizmo for my Sherline milling machine at Cabin Fever and several folks wondered how I aligned the aligner. Having just mounted the counterweight gantry and bashed out a bracket for the pointer, here’s how it went down.
Laser pointer on bracket on counterweight gantry
The blue-gray bracket started life as a shelving support strut. I machined the web from between two holes so I could slide the pointer along the strut, filed off some sharp edges, and mounted the laser pointer with an assortment of machine screws & wing nuts.
I used a plumb bob to figure out roughly where the laser beam must start in order to go straight down the milling machine’s bore, then wiggled & jiggled the strut and pointer to get it more-or-less there. None of this is very precise, but it provides a starting point.
Here’s the trick: put a mirror flat on the mill table. When the reflected spot hits the bezel around the laser’s outbound lens, you know the beam is (pretty nearly) perpendicular to the table. Tweak the pointer’s mounting screws to make that come out right.
Use the plumb bob to figure out where the pointer is in relation to where it should be, wiggle & jiggle & slide everything until it’s there, then tighten & re-jigger everything to tweak the spot location.
Takes about 15 minutes, doesn’t involve any cussing, and works like a champ!
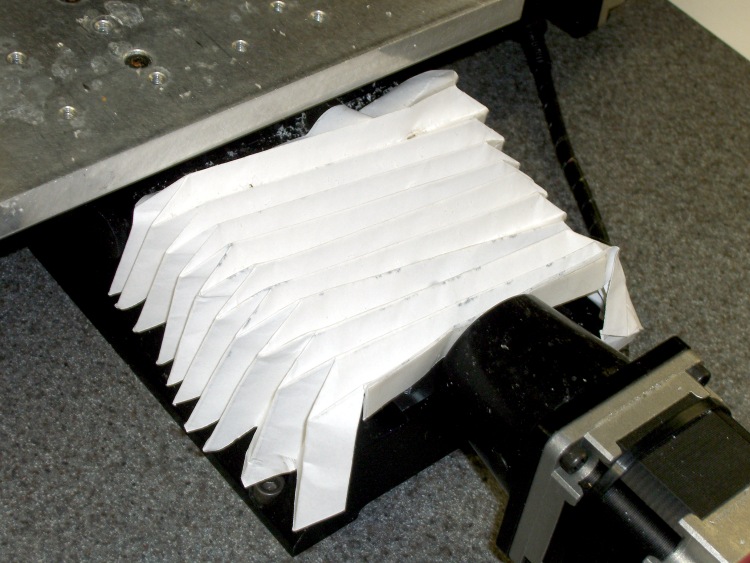
The Y-axis leadscrew on a Sherline milling machine sits exposed to all the crap blowing off the cutter; maybe it doesn’t matter, but it seems nasty.
Throw them out when they're this dirty!
So I made a set of way covers from the template available here or here, except I used plain old printer paper, stuck in place with double-sided tape. The picture shows what one looks like after surviving the rigors of a trip to Cabin Fever Expo.
The key feature is that, when they get too schmutzig, you just throw them away and fold up a new set. It’s easier than dismounting and cleaning something more substantial that you can’t just discard because you’ve developed a serious, deep, long-term emotional attachment.
Everybody at Cabin Fever Expo liked them and wanted the template. If those links have rotted out, I have a copy of the file in the Useful Stuff section: here.
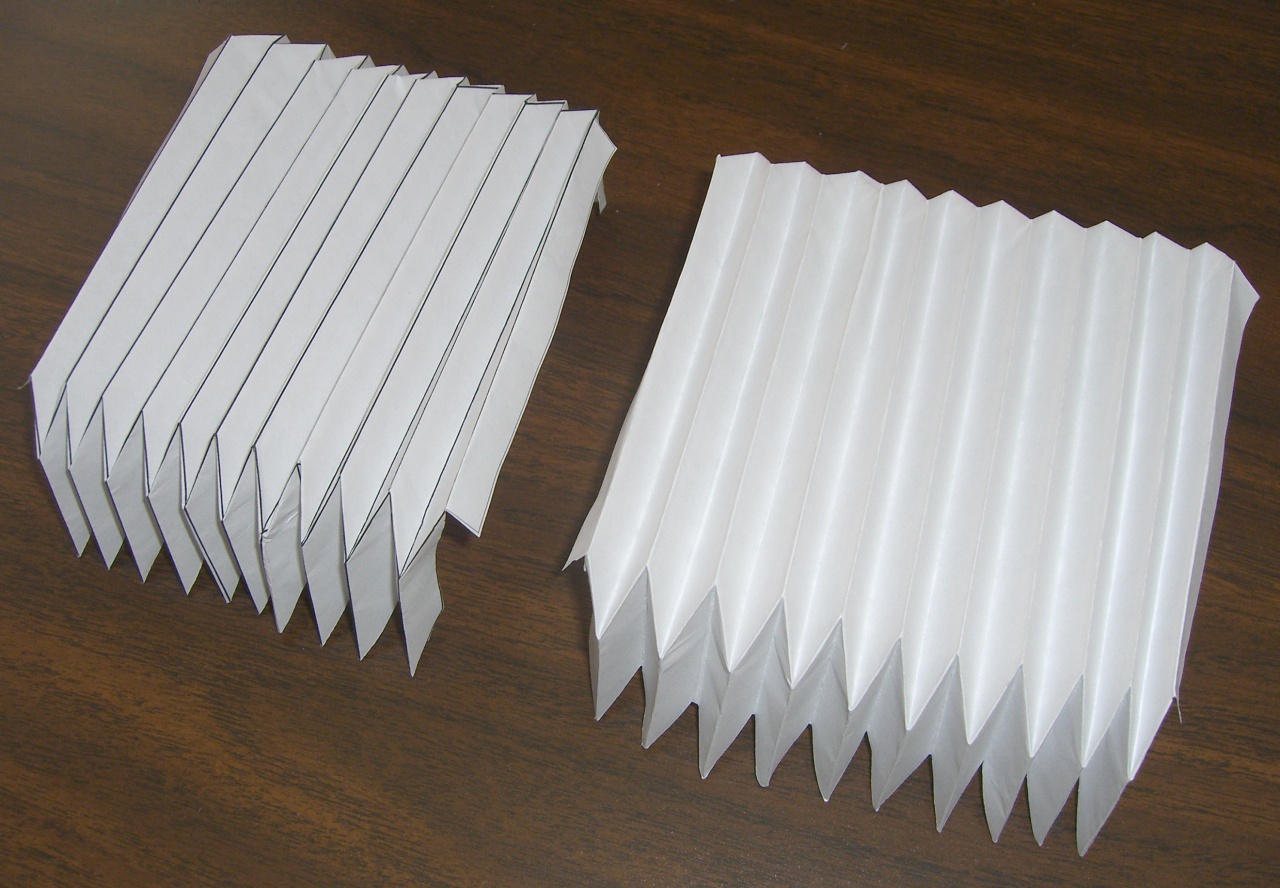
Bellows Folding
Update: Here’s a closeup of a new set. Start with the printed lines up, then fold the end tabs up: the printed side will be down (as in the bellows on the right) and nobody will know how poorly you followed the lines. Click to get a big pic with decent resolution if you need more detail.
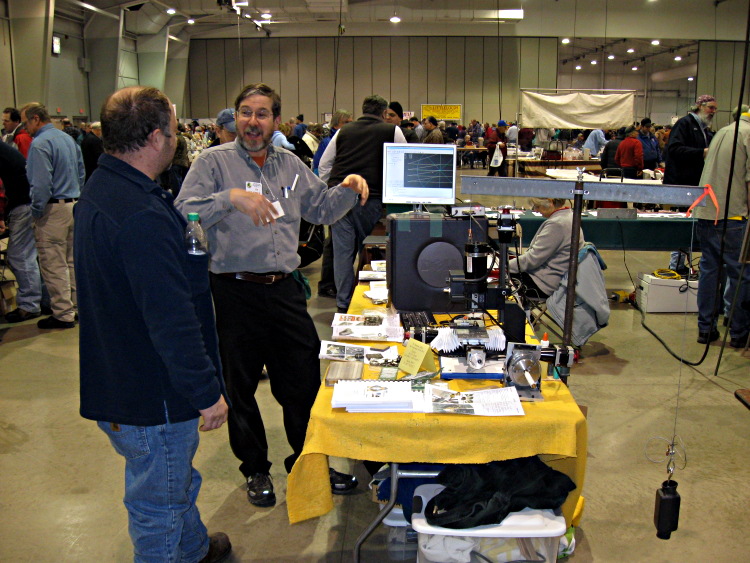
So I hauled my Sherline CNC milling machine gadgetry, an assortment of trivial projects, a stack of handouts with pix & G-code, and a pile o’ EMC2 doc to Cabin Fever Expo for two days of Performance Art…
Ed Nisley Demo-ing CNC at Cabin Fever. Picture courtesy of Brian Glackin.
The key is to have the knobs turning: an inactive machine is just background clutter that everyone walks right past. It’s not nearly as interesting as miniature tools or a chuffing steam engine.
There’s something to be said for being on the crowd side of the table, as that lets both of you see the monitor. A bigger display might be more helpful; I duct-taped a 14-inch 1024×768 LCD panel to the top of the desktop PC box.
Although I brought some blank stock along, it quickly became obvious that live-fire milling under show conditions is a Bad Idea: far too many distractions and far too many things can go wrong. So I contented myself with cutting air; nobody really minded and I could switch programs in mid-stride to show folks the G-code program they really wanted to see.
Plenty of folks stopped by, many of whom either have CNC running or are in the throes of getting started. A surprising number of conversations started with “I have this old Bridgeport …” and went on from there.
There’s a crying need for a comprehensive machine design tutorial that explains how all the pieces fit together, with sort of a flowchart outlining the choices (I know it’s more complex than that, but a diagram would be a starting point for discussion). I don’t know enough of the servo end of the biz, but someone should show how the machine’s size determines the motor size and, thus, the motor driver size, with plenty of examples. There’s a misconception that you can run a big machine on little steppers or puny servos, with the controller making up the difference.
Many people do not understand the difference between CAD, CAM, and what EMC2 provides. I described the process as three layers: CAD makes the pretty pictures, CAM digests those pictures and emits G-code, EMC2 converts G-code into motion. That seemed to help.
The single most attention-getting part of the exhibit was, to my astonishment, my Orc Engineering counterweight (described here and here) supporting the Sherline’s milling head. I had to explain just exactly why you need a counterweight in the first place (heavy offset motor, short Z-axis ways) and how much it weighs (13 pounds, a bit too much). Some folks commented that they put similar counterweights on their much larger machines and after a while I stopped feeling inadequate.
EMC Penguin Mascot
At least a dozen people picked up my EMC doc and asked if I was selling it; took me a while to realize they wanted to buy the booklets. I don’t know if you could make any money at it, but there’s a definite market for ink-on-paper books with no plot and weak character development. Now, if Chips were was way more shapely, we could have a real bodice-ripper cover. Somebody get on that, OK?
I make booklets using Adobe Reader’s print-as-booklet feature, a printer with continuous-flow inking, and an Ibico comb binding machine, but there’s enough fiddling that doing much of it for anybody else just doesn’t make sense. Something like Lulu might work, but there’s a stiff (to me, anyway) up-front charge and the EMC doc changes often enough that you’d have to run plenty fast to stay in the same place.
Other people picked up the books and asked if I was selling the software. They seemed puzzled when I said it was free for the download and that not only was the software free, but the GPL meant that they were, too. I need to work on that part of the schtick… should’a had a few CDs to pass out, too.
I remembered to bring a bag of cough drops, ate ’em like candy, talked almost continuously, and wound up hoarse anyway. Probably convinced a few folks to try EMC, didn’t terrify many children, and a good time was had by all.
Although live-fire milling is scary, it’d be fun to make something like a finger ring (as in Dan Statman’s gorgeous designs, but plastic) as a hand-out freebie. The whole process should take no more than five minutes, tops, which might be tough. Running a rotary table and the mill would be a real crowd-pleaser; my 4th axis attracted some questions. Perhaps an EMC tag-team would suffice: one to mind the mill while the other works the crowd?
As always, Cabin Fever is stuffed with gorgeous examples of machine-shop work. Those guys actually know what they’re doing; I can write G-code, but it’ll take many more years of experience before that code actually makes passably pretty parts.
The first thing you do in any CNC milling setup is to locate the part’s origin to the spindle axis. Big mills use homing switches and carefully calibrated fixtures. I used to stick a pointy carbide scribe in a collet, push it finger-tight into the spindle, and align by eyeballometric guesstimation.
That actually works pretty well for most of my projeects, as a few mils (heck, a few dozen mils) one way or the other doesn’t make much difference.
I kept lusting after an SDA Laser Center / Edge Finder (as advertised in Home Shop Machinist), which a friend says works really well. They have a 1/4″ (6 mm) shank for smaller machines, but it’s still nigh onto three inches long and headroom is a precious commodity in a Sherline mill.
I’ve seen projects using laser pointers as alignment tools, usually with an intricate six-axis gimbal hoodickie to aim the beam in exactly the right direction. If you’ve ever sighted along the body of a hand-held laser pointer, you’ll quickly see that the laser chips and optics project the beam in a generally forward direction, but any alignment is purely coincidental.
Then I had an insight: the spindle always stays aligned along one vertical axis. The mill is firmly bolted to the table, the table to the concrete-block wall, and the floor joists overhead rest on the wall, which means a laser mounted on a floor joist could shine right down the spindle bore. Do all the fiddly alignment once, then it’ll Just Work forever after.
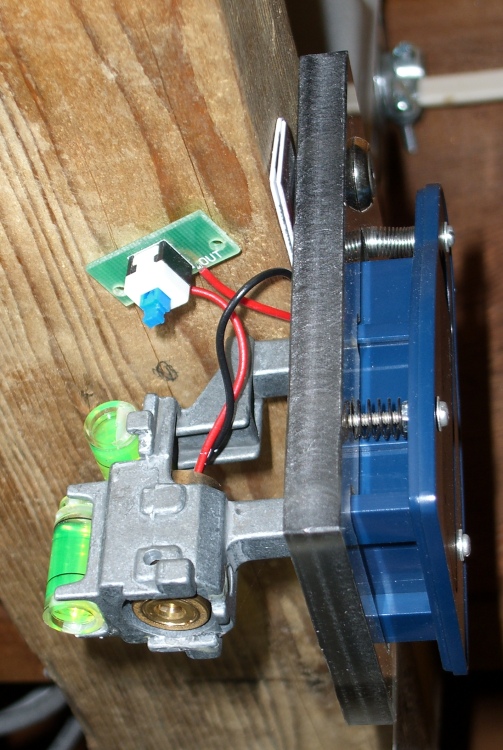
The top picture shows the result. A cheap-after-rebate (ten bucks, tops) Sears carpenter’s laser level provided the guts of the project; it’s no longer available, but you get the general idea. The fancy housing includes a cylindrical lens that converts the dot into a line, but stripping off the housing gets rid of that unwanted feature.
I carved out a plastic base plate and tapped it for 2-56 screws for fine adjustments. They fit directly in the holes that originally held the top of the housing, with springs to hold the level in position.
A plumb bob showed that the level had to live about halfway between two joists, so I screwed a scrap of 2×4″ in place and then screwed the level to that. The cardboard shims reveal the fact that the side of the board isn’t vertical, but I doubt cutting it would have helped much. After that, it’s a matter of sliding it this way & that, tweaking the screws, and fiddling around until the beam falls straight down the middle of the spindle.
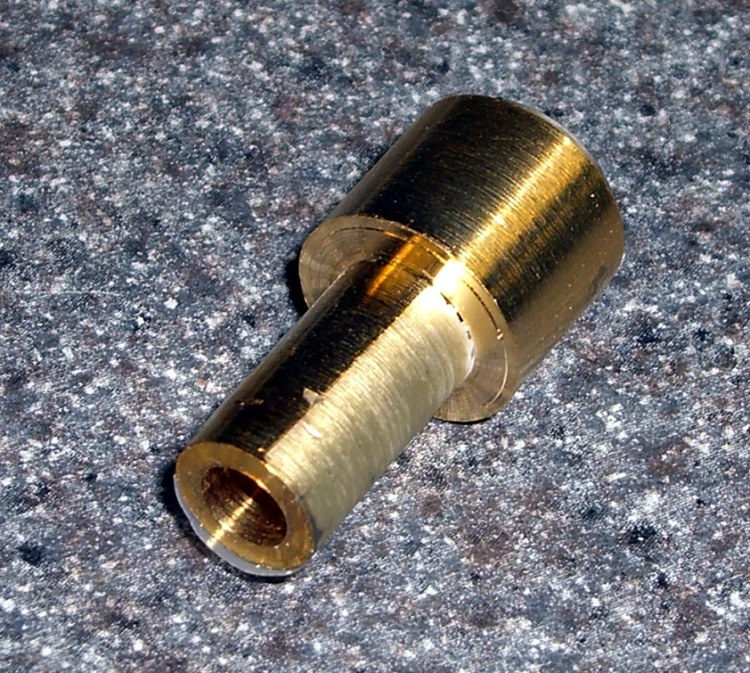
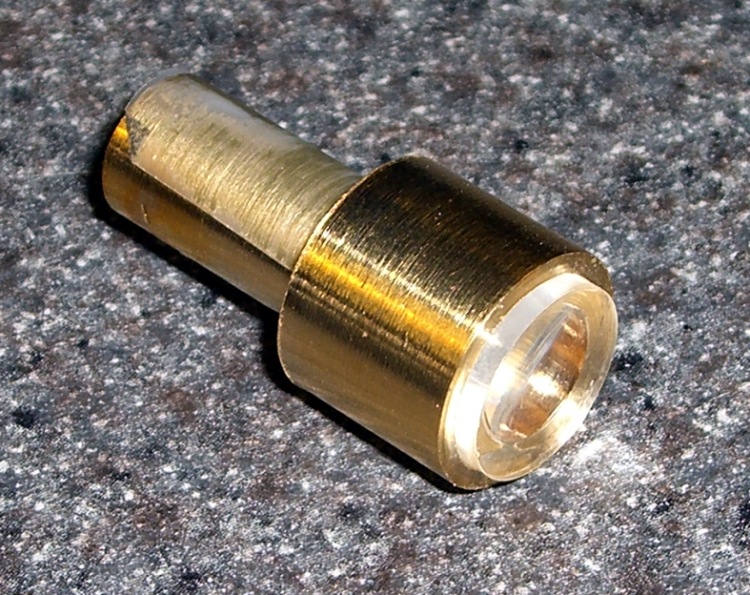
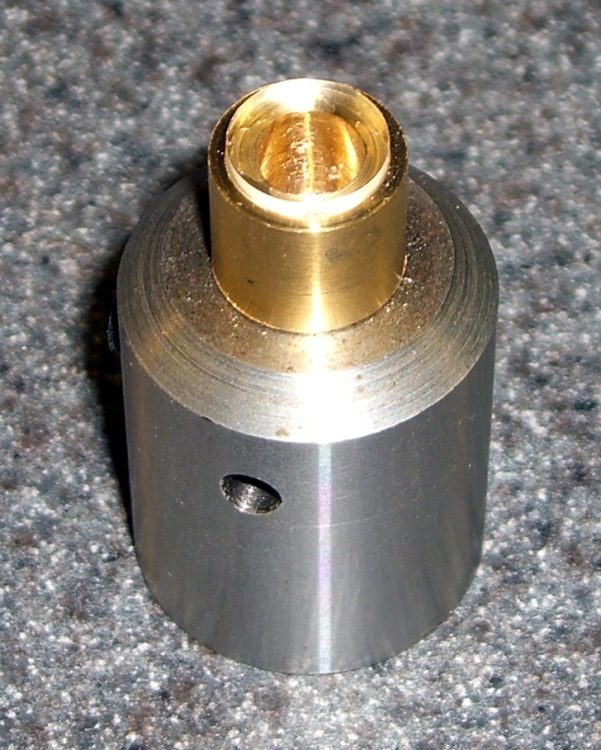
The laser spot is far too large, but a small lens will do the trick. Long ago I got a sack of small lenses from a surplus outlet that included a teeny plastic lens with a 1-inch focal length. A bit of lathe work turned out a holder with a bore just a bit larger than the laser spot.
The hole trims off all the junk light around the spot itself and cuts it down to a few mm in diameter, well-centered on the spindle axis. You can’t get too skinny here, as diffraction gets in the way, but the holder bore presents a decent spot to the lens.
A dot or three of cyanoacrylate adhesive (I just hate the term “crazy glue”, don’t you?) holds the lens in position. As long as the lens is centered and reasonably perpendicular to the axis, it’ll work fine. The lens is much larger than the spot, so you could use one that’s even smaller than this with impunity.
The narrow shank fits into an end mill holder, of which you should have several anyway, and the wrap of tape makes it a snug slip fit. If I hadn’t tried to get clever, the brass would be the right diameter; I keep telling myself to make another one and some day I will.
Because the beam is essentially parallel, the lens focuses it to a brilliant spot about 1 inch below the lens.
The maximum angular error (offset from the true spindle axis) is pretty small, no matter how bad a job you do, because the beam must pass through the middle of a 10-mm tube that’s 130 mm long. Assuming it’s slanted off-axis by 1 mm at the top and still makes it into the hole in the lens holder, that’s under half a degree. At the far end of the 1-inch focal length, the spot is off-position by 9 mils, call it 0.2 mm.
However, the lens focuses that beam down by a pretty good factor and reduces the error by the same factor. I don’t have the number, but in practice I think the spot size is larger than the alignment error.
You can do better than that by adding another aperture at the top of the spindle and getting really fussy with alignment.
In any event, it’s closer than I came with the carbide scriber!
Update: I mounted it on a new bracket attached to the new counterweight gantry: much better! Some tips on aligning the thing there.
The motor driver box on my Sherline mill started out as a stock unit, but I’ve tweaked the circuitry to improve the analog performance. Those adventures formed the basis of my Above the Ground Plane columns in Circuit Cellar magazine columns for August & October 2004.
Because the firmware for the PIC microcontrollers wasn’t available, I wrote a clean-room version so I could show how it all worked for the column. My code won’t run on a stock Sherline board, though, so it’s not a drop-in replacement for the stock firmware.
One of the reasons I attacked the controller was to reduce the audible noise coming from the motors. That’s an inescapable part of chopped-current stepper motor drive circuitry, but the noise was modulated by all manner of things that shouldn’t have affected it; just touching the box shouldn’t make any difference at all. The fact that it did meant the circuit board had some, well, infelicitous layouts.
Although the final result was much more stable, I decided to turn off each motor if it didn’t move for at least five seconds; that’s a simple firmware tweak when you write your own code. As a result, the shop was quiet when I wasn’t actively milling.
Solar Measurements Circuit Board – Top Side
Now, having a motor be completely turned off while milling is going on isn’t generally a good idea, because milling forces from the other axes can push the table against the leadscrew and, perhaps, turn the screw against the unresisting motor. I figured that on a Sherline mill, what with the sissy little cuts I take, that wouldn’t be a problem.
And I was right for the better part of four years!
A benefit of turning the driver circuitry off was that I could easily twist the knobs by hand to fine-tune the XYZ position during setup. That worked out really well.
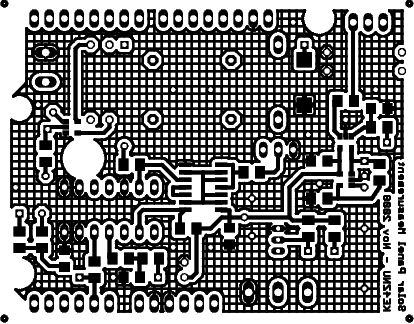
However, drilling the seemingly simple circuit board pattern you see here (for my February 2009 CC column) produced exactly the right collection of forces (while drilling? Huh?), vibration (maybe) and motor pauses (for sure) to introduce an absolutely repeatable positioning error that Went Away when I tweaked the firmware to keep the motors enabled at all times.
I’ve since made another tweak that reduces the current to an idle level after five seconds. That both reduces the audible noise and drills the board correctly, so I’ll keep an eye on it for a while before declaring victory.
The PCB has a few unused (in my code, anyway) chip-to-chip connections that I could employ to let them all decide when nobody’s moving. I think turning the motors off 20 seconds after the last axis stops moving should work Just fine; my G-code doesn’t wait around that long except for manual tool changes.
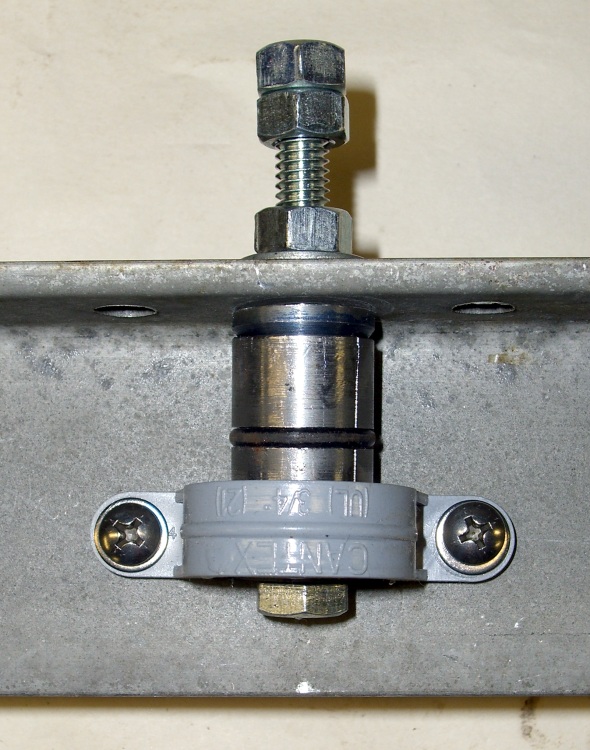
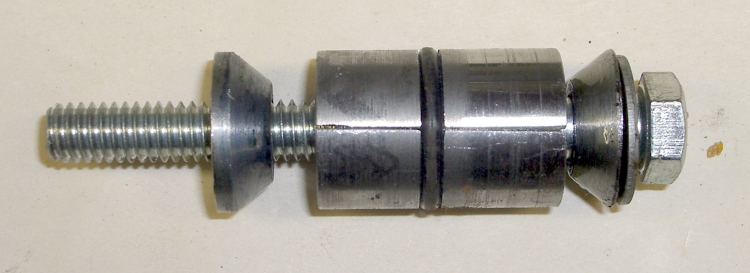
This is the dingus that attaches the crossbeam to the central pipe rising up from the table for my counterweight gantry. I discarded a whole bunch of elaborate construction ideas in favor of just jamming a plug in the pipe and cranking down on a nut to tighten it.
Expanding plug overview
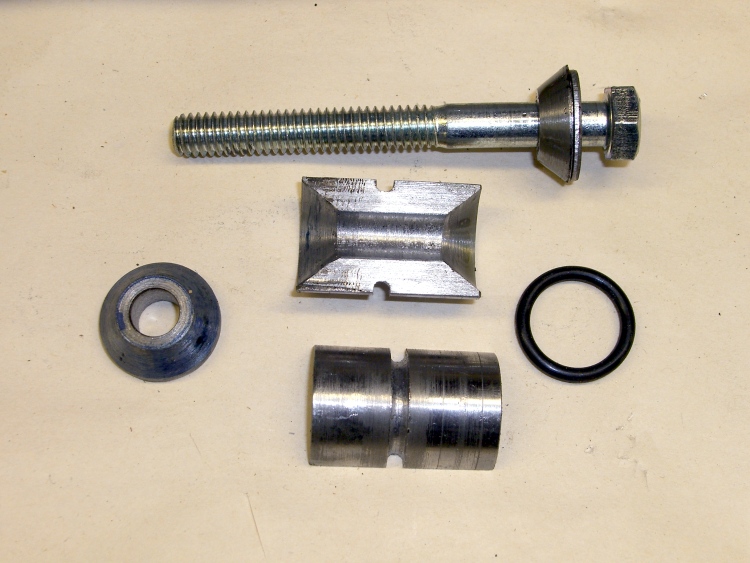
It’s pretty much self-explanatory; I cut everything to fit, cleaned up the cuts with a file, and added some lube to the tapers so as to make it nice & slippery.
The need for an O-ring to hold the halves together occurred to me after I’d bandsawed a 1 mm trench in the side of the plug. I chucked it up in the lathe again and used a round-nose tool to carve a groove around its belly. If you try this, do the groove first: an interrupted cut is murder on what’s basically a parting-off tool.
Expanding plug parts
While I know (thanks to Guy Lautard’s invaluable Machinist’s Bedside Reader books) that a self-releasing plug must have a taper angle with a tangent greater than the joint’s coefficient of friction, that really wasn’t much help here. I picked 40 degrees and, yup, it’s self-releasing, but not really slippery enough. Takes a bit of torque to expand the plug enough for a good grip.
Perhaps my grubby surface finish has something to do with it?
Memo to self: find out how to figure the taper angle correctly, then do better finishing.
 The Smell of Molten Projects in the Morning
